
Plating Process
Electroforming vs Electroplating: Key Differences
Electroplating coats a part; electroforming grows the part itself. Compare purpose, precision, tooling and the equipment behind each process.
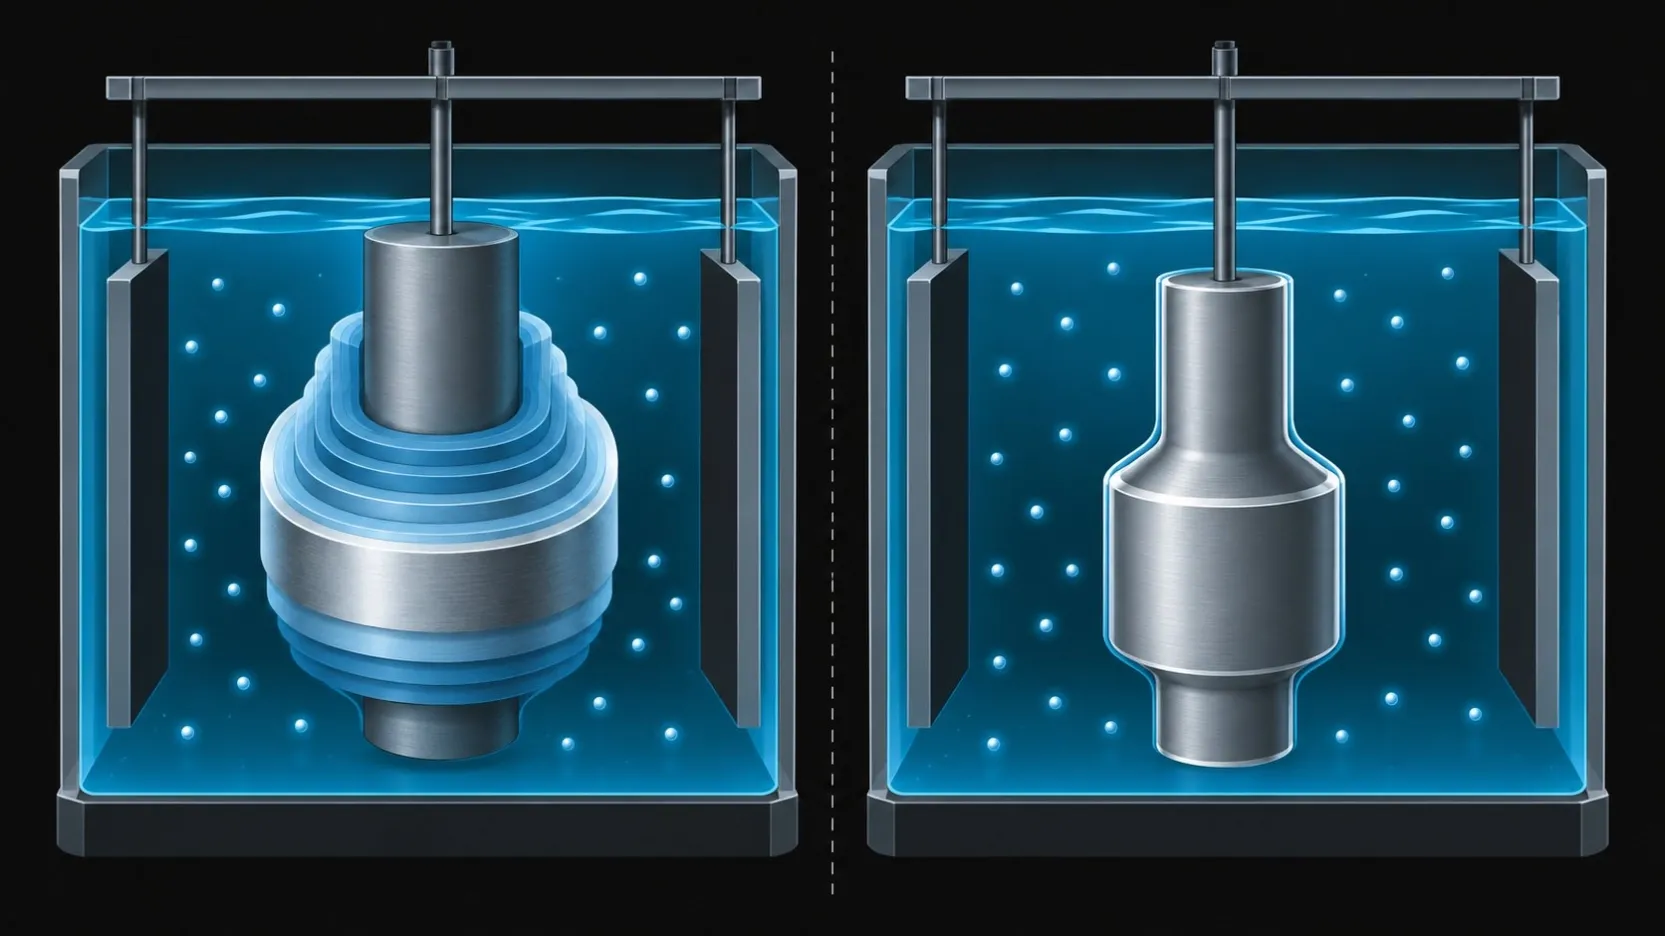
Electroplating coats a part that already exists; electroforming grows the part itself on a mandrel until the deposit becomes the product. About a 6-minute read.
Same electrochemical physics, opposite purposes — the choice changes tooling, cycle time and equipment.
Written by Nick Wong · Engineering reviewed by Li Wang · Published 3 October 2026 · Updated 3 October 2026
The Core Difference
In electroplating, the substrate is the point: a conductive part is coated to give it corrosion resistance, wear resistance, solderability or appearance, and the deposit is measured in micrometres. The part leaves the line as itself, improved.
In electroforming, the mandrel is the starting point: metal (typically nickel or copper) is deposited onto a carefully prepared mandrel — metallic or non-conductive and metallized — over hours, until the deposit is thick enough to be separated from the mandrel and stand alone as a precision metal part. Foils, meshes, bellows, optical reflectors, micro-precision components and mould inserts are classic electroformed products, valued for geometry fidelity that machining struggles to match on thin or intricate shapes.
Comparison Table
Aspect | Electroplating | Electroforming |
|---|---|---|
Purpose | Coat an existing part | Grow the part itself |
Deposit thickness | Micrometres, per spec | Tens to hundreds of micrometres — the part's wall |
Substrate | The production part (stays) | A mandrel (removed or stayed-in for some products) |
Time per load | Minutes to an hour | Hours |
Geometry role | Follows the part surface | Replicates the mandrel surface in fine detail |
Typical metals | Zinc, nickel, copper, tin, chrome | Nickel, copper (nickel most common) |
Line emphasis | Pre-treatment, rectifiers, rinsing | Mandrel preparation, ultra-stable chemistry, long-cycle control |
Choosing Between Them
Ask one question: is the metal a coating or the component?
- If you need to protect, harden, solder or beautify an existing part — electroplating, with the process chosen per the comparison of applications.
- If you need to produce a thin, intricate, high-fidelity metal component that would be difficult to machine or stamp — electroforming, or a precision stamping/etching route, depending on volume and tolerances.
Volume matters: electroforming is a slow, high-precision process; high volumes of simple thin parts usually belong to stamping, with electroforming taking the intricate or ultra-precise end of the range.
What the Equipment Looks Like
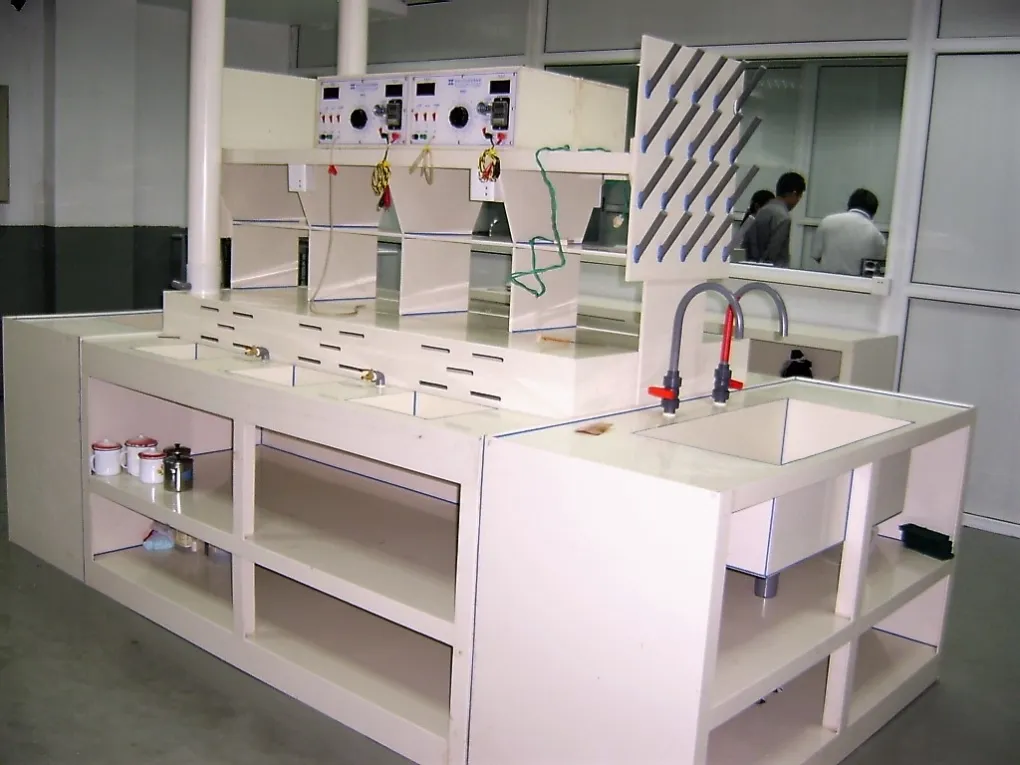
Both are DC electrodeposition lines — plating equipment of the same families: solution tanks, rectifiers, filtration, temperature control and the standard process skeleton. Electroforming lines emphasize what long deposition cycles demand: exceptionally stable bath chemistry and temperature, mandrel preparation and release stations, slow agitation that does not disturb fine growth, and cycle control measured in hours rather than minutes.
Standards and Evidence Boundary
- ASTM B832 — electrodeposited copper electroforming; an example of process-specific standards in this field.
- Chemistry supplier datasheets — bath windows and deposit properties are defined there.
- Your part geometry and tolerances — the deciding evidence; electroforming capability is quoted per part, not generically.
Evidence boundary: this article explains the two processes at industry-general level. Achievable precision, cycle times and deposit properties come from the chemistry supplier and process capability data — not from this page.
FAQ
Is electroforming a type of electroplating?
Electrochemically yes — both deposit metal under DC current. Industrially they are separate disciplines: electroplating coats parts, electroforming manufactures them. Suppliers, equipment emphasis and quality control differ accordingly.
Why is electroforming slow?
Because the deposit is the product: building a self-supporting wall of metal takes hours of controlled deposition. The slowness is the price of geometry fidelity on thin, intricate shapes.
Can electroformed parts be made in high volume?
Electroforming lends itself to batch and continuous mandrel processing for repeatable small parts, but for simple geometries at high volume, stamping and etching are usually more economical. The intricate, high-precision end is where electroforming wins.
Related Reading
- Pillar guide: What Is Electroplating? — the process family both belong to.
- Adjacent decision: The Electroplating Process, Step by Step — the skeleton both lines run.
- Next step: browse plating equipment — tank lines, rectifiers and handling for deposition processes.
Diagnostic CTA: What to Send Us — and What You Get Back
Send your part drawings and process goal through our RFQ form — geometry, tolerances, volumes and substrate situation. ES-PRO returns: an assessment of which deposition route fits, a line concept for it, a quotation, and an explicit list of open questions — we state what is missing rather than assuming it.
References & Authorities
- ASTM B832 — Guide for electroforming with copper and nickel — ASTM International.
- Chemistry supplier datasheets — bath windows and deposit properties are defined by the chemistry supplier.
- Industry associations — e.g., NASF (National Association for Surface Finishing, US) and IMF (Institute of Materials Finishing, UK) publish supplementary guidance and training for the surface-finishing industry.
Standards are cited for identification; always use the current edition from the issuing body. Process parameters are governed by the datasheets for the specific chemistry.


