
Plating Process
The Electroplating Process Explained Step by Step
The industrial electroplating process step by step: degreasing, acid pickling, activation, plating, rinsing, post-treatment and wastewater handling.
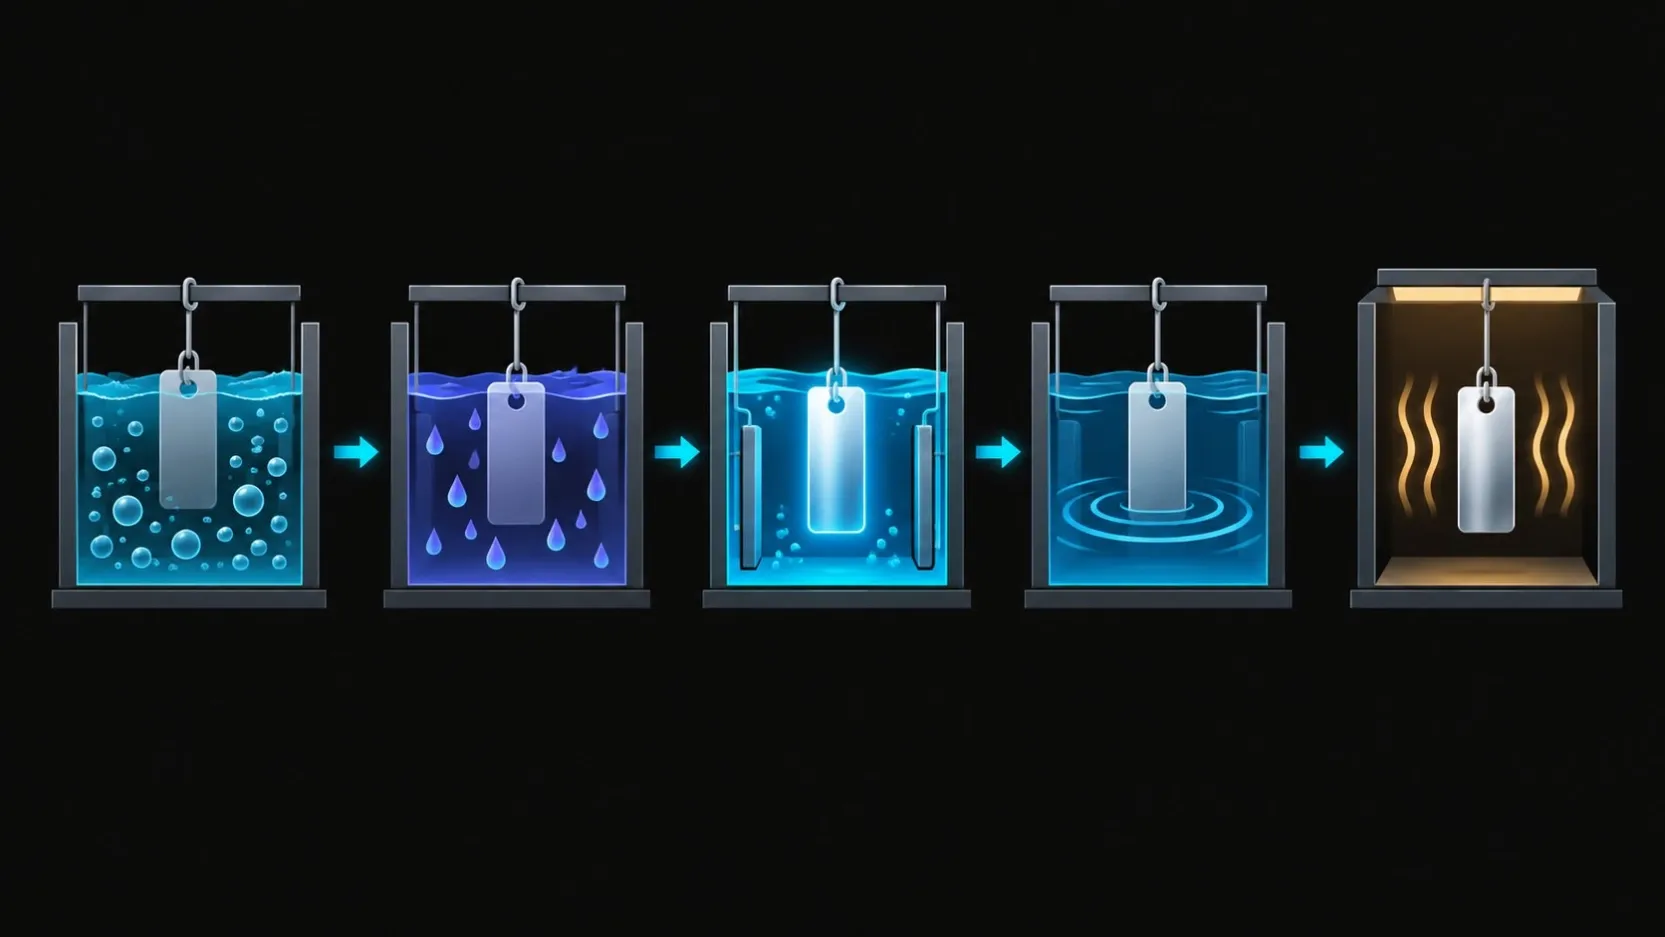
A walk-through for process and quality engineers: the ten steps of an industrial plating line, what each one does, and why pre-treatment decides the outcome. About a 7-minute read.
Written by Ivy Deng · Engineering reviewed by Ben Yuan · Published 2 October 2026 · Updated 2 October 2026
The industrial electroplating process runs in three stages: pre-treatment removes oil, oxides and scale so the coating can adhere; the plating stage deposits metal under tightly controlled DC current; and post-treatment rinses, neutralizes, dries and treats wastewater. Most coating failures trace back to shortcuts in pre-treatment — not to the plating bath itself.
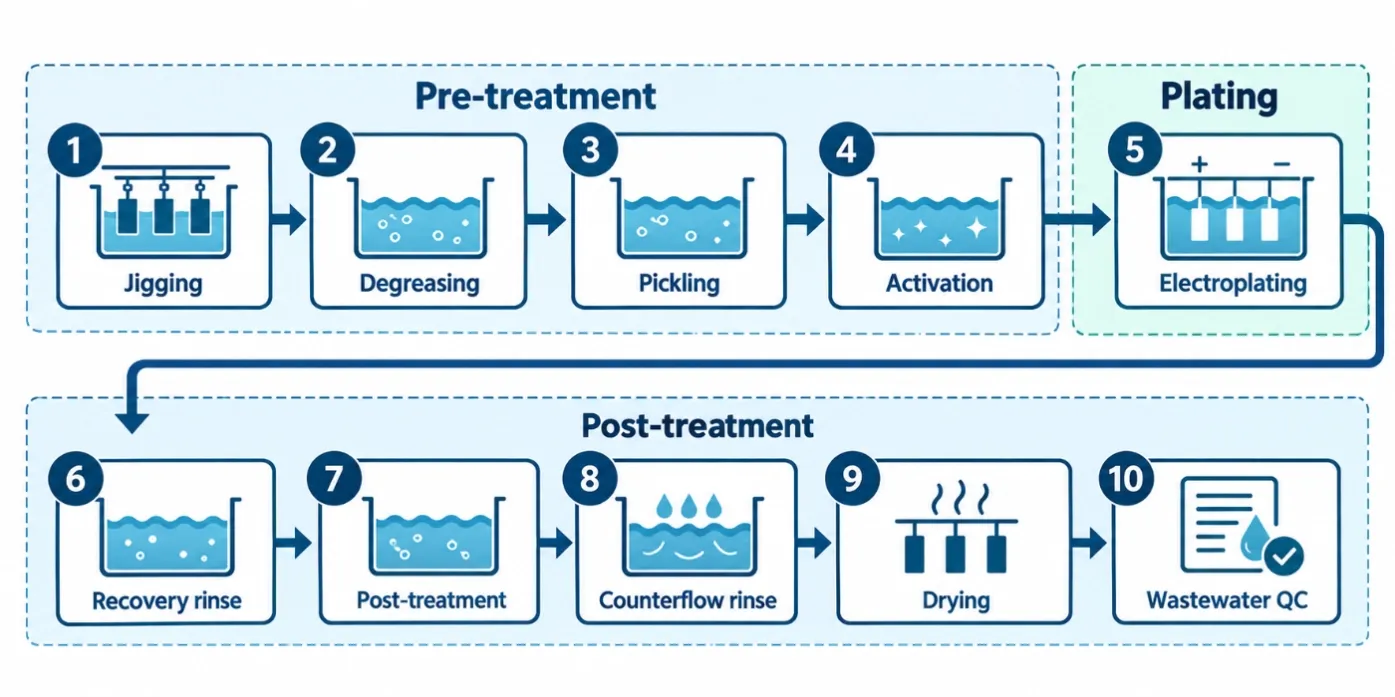
The Line at a Glance: The 10 Steps
- Jigging and loading — parts are mounted on racks or loaded into barrels
- Degreasing — oils and greases are removed (soak, ultrasonic or electrolytic)
- Acid pickling and descaling — oxides, rust and scale are stripped
- Surface activation — a final light acid dip prepares the surface for bonding
- Electroplating — the actual metal deposition under DC current
- Drag-out recovery and first rinse — chemistry is reclaimed, contamination removal starts
- Post-treatment dips — neutralizing, passivating or anti-tarnish
- Multi-stage counterflow rinsing — final rinse stages for spot-free surfaces
- Drying — hot air or centrifugal, immediately after rinsing
- Wastewater treatment and quality control — rinse water is treated and coatings are verified
The load is rinsed between every chemical stage; steps 6 and 8 describe how modern lines handle that rinse water systematically.
Steps 1–4: Pre-Treatment — Where Quality Is Won or Lost
Step 1 — Jigging and loading. Parts are fixed onto racks or loaded into plating barrels with two goals: electrical contact must be reliable, and every surface must face the solution so current distributes evenly. Bad jigging shows up later as thin spots and burn marks — rack design is engineering, not an afterthought.
Step 2 — Degreasing. Machining oils, drawing compounds and fingerprints repel aqueous plating solutions. Alkaline soak cleaning, ultrasonic cleaning or electrolytic degreasing (where the part gas-evolves to scrub the surface) removes them. Miss any oil film and the plating solution cannot wet the surface — the deposit there will peel.
Step 3 — Acid pickling and descaling. Oxides, heat-treat scale and rust physically block deposition. Acid pickling dissolves them; the choice of acid and inhibitors depends on the substrate so base metal is not attacked.
Step 4 — Surface activation. Immediately before plating, a short acid dip removes the microscopic oxide film that re-forms on cleaned metal within minutes. Plating must follow activation quickly: an active surface is the handshake the deposit bonds to.
This is why pre-treatment dominates quality: a deposit plated over residual oil, oxide or scale looks fine coming out of the bath and fails weeks later as blistering or peeling. Field experience across the industry is consistent — the majority of adhesion complaints trace back to pre-treatment, not to the plating bath.
Steps 5–6: The Plating Stage
Step 5 — Electroplating. The rack or barrel enters the plating tank, where the part is the cathode and DC current from a plating rectifier drives metal ions from the solution (and usually from dissolving anodes) onto the surface. Deposition rate and coating grain are governed by bath chemistry, current density and temperature. Typical industry ranges run from a few to a few tens of amperes per square decimetre of cathode surface, and many common baths operate between ambient and around 60 °C — actual recipes are set by the chemistry supplier for the specific coating system. Agitation and continuous filtration keep the bath uniform; temperature control (heating, or chillers where heat builds up) keeps it stable.
Step 6 — Drag-out recovery and first rinse. When the load leaves the tank it carries solution with it — drag-out. A recovery or first rinse captures as much of that chemistry as possible, both to stop contamination moving downstream and to return valuable metal to the process. This step is also where cost control lives: every millilitre of drag-out is chemistry that must be replaced and wastewater that must be treated.
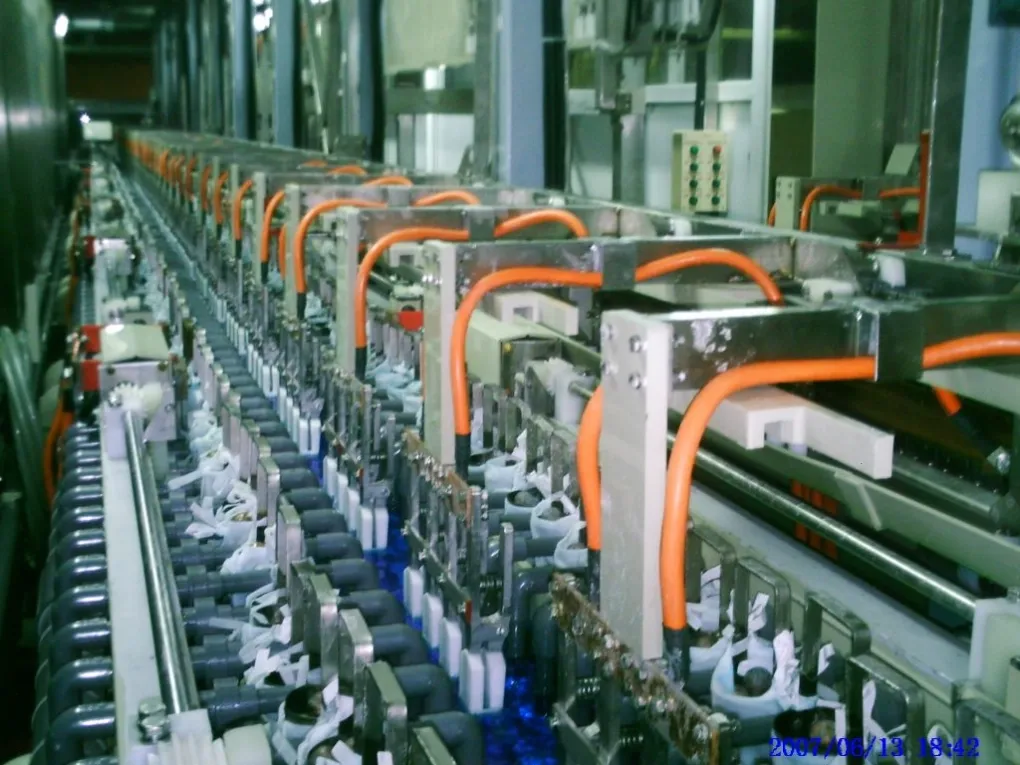
Steps 7–10: Post-Treatment, Rinsing, Drying and Water Care
Step 7 — Post-treatment dips. Depending on the coating system, the load may be neutralized, passivated or given an anti-tarnish treatment. Zinc coatings, for example, receive a chromate conversion layer (today usually trivalent) that multiplies corrosion resistance and sets the finish colour.
Step 8 — Multi-stage counterflow rinsing. Modern lines rinse in several stages where water flows opposite to the parts: the load meets progressively cleaner water, and the freshest water is used last.
Step 9 — Drying. Hot-air dryers or centrifugal dryers remove rinse water immediately, before minerals or chemistry traces can dry as spots on the surface.
Step 10 — Wastewater treatment and quality control. Rinse water and spent baths are treated before discharge, and coatings are verified — thickness measurement and adhesion tests confirm the line is holding spec. Dedicated plating wastewater treatment is a permanent stage of the process, not an external service.
Field Workflow: The Rinse Math Every Line Runs On
A reusable rule for rinse design: each counterflow rinse stage multiplies the dilution of drag-out carried forward. As a planning rule of thumb, a well-built counterflow stage reduces contaminant concentration by roughly one order of magnitude, so a three-stage counterflow rinse leaves the part roughly 1,000× cleaner than a single-rinse exit — with far less water than three separate rinses, because the stages reuse water flowing the opposite way.
Process audit checklist (walk any line against it):
- ☐ Rinsed between every chemical stage — no direct tank-to-tank transfers
- ☐ Counterflow direction verified: water flows against part movement, freshest last
- ☐ Drag-out recovery or first rinse present after every valuable bath
- ☐ Bath temperature, level and filtration alarms wired to the operator panel
- ☐ Thickness and adhesion checks scheduled per shift, not per complaint
Standards and Evidence Boundary
References buyers and quality engineers commonly cite around this process (always the current edition):
- ISO 2080 — Electroplating and related processes: vocabulary; aligns process-step terminology across suppliers and audits.
- ASTM B633 — Electrodeposited zinc coatings on iron and steel with thickness classes by service condition; the model for the spec the line must hold at step 5.
- ASTM B568 — X-ray spectrometry measurement of coating thickness; the standard QC method behind step 10 thickness numbers.
- Local discharge permits — the legal boundary that step 10 exists to satisfy.
Evidence boundary: this article gives process-general facts and textbook parameters (current density and temperature as typical industry ranges). Bath recipes, chemistry windows and discharge limits come from the chemistry supplier's datasheet, the applicable coating standard and your local authority — not from this page.
FAQ: Process Questions Engineers Ask
Why do electroplated coatings peel or blister?
In most cases the deposit bonded to a contaminant instead of the metal — residual oil, an oxide film or scale left by incomplete pre-treatment. Correct degreasing, pickling and immediate activation prevent the overwhelming majority of adhesion failures.
How long does the full electroplating process take?
Individual tanks run from a few minutes (activations, rinses, thin deposits) to around an hour (thicker deposits). A full pass through pre-treatment, plating and post-treatment for typical protective or decorative work completes in well under an hour of tank time; heavy engineering builds take proportionally longer.
What is current density, and why does it matter?
Current density is the DC current per unit of cathode surface area, and it controls both deposition speed and coating quality. Too low wastes tank time; too high burns or roughens the deposit. It is the single most-tuned parameter in the plating stage.
Why do plating lines have so many rinse tanks?
Counterflow rinsing multiplies dilution: each stage dramatically reduces the chemistry carried into the next, which protects downstream baths, delivers spot-free surfaces and cuts both water consumption and wastewater volume at the same time.
Related Reading
- Pillar guide: What Is Electroplating? — the definition, coating types and line anatomy behind this sequence.
- Adjacent decision: How to Set Up a Metal Plating Line — turning this process into a tank-by-tank equipment list.
- Next step: browse plating line equipment — every step above maps to a machine category.
Diagnostic CTA: What to Send Us — and What You Get Back
If you're mapping this process onto real equipment, send three inputs through our RFQ form:
- Your process sequence today (or the coating target if starting fresh)
- The step that limits you — throughput, quality, water use or compliance
- Part mix and capacity target
ES-PRO returns: a tank-by-tank line concept that executes this exact sequence, sizing for each stage (rectification, filtration, temperature, rinsing), a quotation, and an explicit list of open questions — we state what is missing rather than assuming it.
References & Authorities
- ISO 2080 — Electroplating and related processes: vocabulary — International Organization for Standardization (ISO).
- ASTM B633 — Electrodeposited coatings of zinc on iron and steel — ASTM International.
- ASTM B568 — Measurement of coating thickness by X-ray spectrometry — ASTM International.
- Chemistry supplier datasheets — bath systems, concentrations and operating windows for specific plating chemistries (issued by the chemistry supplier).
- Industry associations — e.g., NASF (National Association for Surface Finishing, US) and IMF (Institute of Materials Finishing, UK) publish supplementary guidance and training for the surface-finishing industry.
Standards are cited for identification; always use the current edition from the issuing body. Process parameters are governed by the datasheets for the specific chemistry.


