
Plating Process
Ultrasonic vs Vapor Degreasing: How to Choose
Ultrasonic cleaning and vapor degreasing both remove oil and chips. See how they differ in mechanism, throughput, chemistry and the lines that run them.
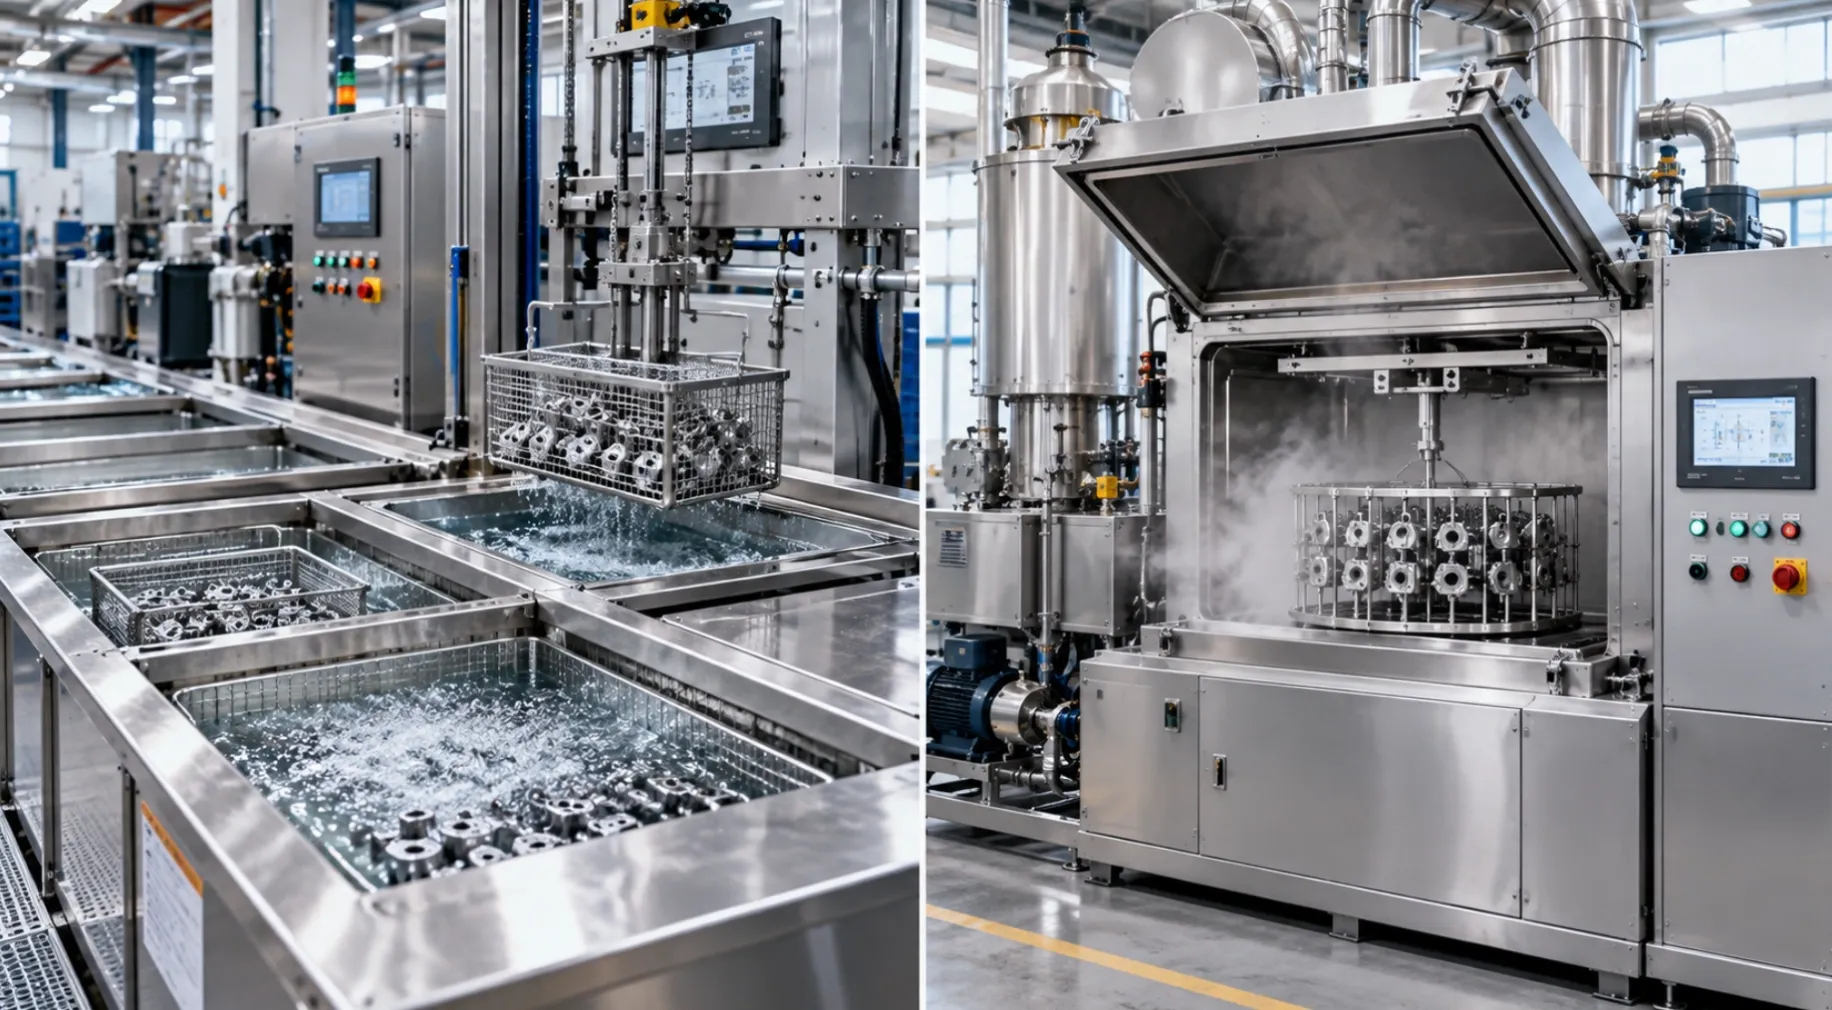
Both remove oil and chips; ultrasonic scrubs with cavitation in water-based chemistry, vapor degreasing condenses pure solvent onto the part. The part and the throughput decide. About a 6-minute read.
Written by Mia Shang · Engineering reviewed by Li Wang · Published 4 October 2026 · Updated 4 October 2026
Degreasing is the step every machining and assembly shop argues about. The two industrial workhorses — ultrasonic aqueous cleaning and vapor degreasing — reach clean surfaces by completely different mechanisms, and each wins in a different part mix.
Two Mechanisms
Ultrasonic cleaning fills a tank with water-based detergent and drives piezoelectric transducers at ultrasonic frequency; cavitation bubbles form and collapse against every wetted surface, lifting oils, chips and polishing compounds out of blind holes and joints. It is a batch or conveyor flow: wash → rinse → dry. The physics are in how ultrasonic cleaning works, and water quality matters — see distilled vs deionized water for the rinse side.
Vapor degreasing boils a solvent; parts descend into the solvent vapor zone, where vapor condenses on the cooler metal and dissolves oil off the surface, then a rinse sump and vapor drying finish the job. No mechanical action beyond condensation and gentle boiling — the solvent does the work.
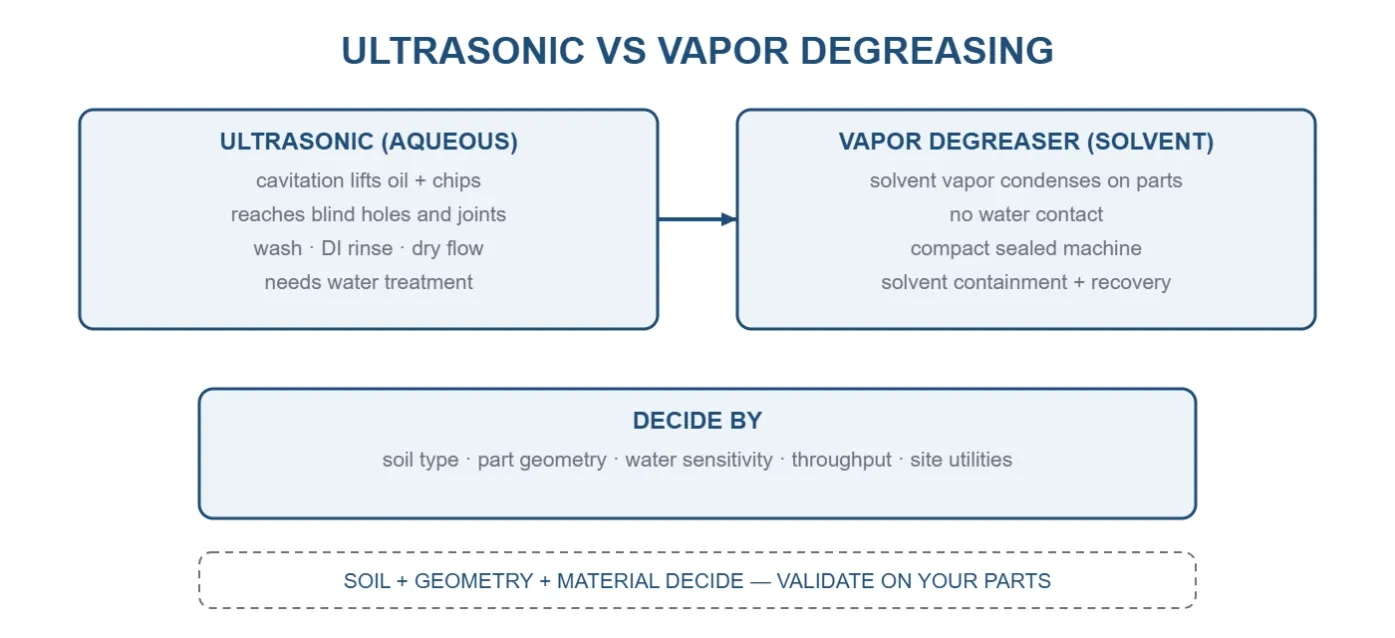
Comparison: Reference Table
Aspect | Ultrasonic (aqueous) | Vapor degreasing (solvent) |
|---|---|---|
Mechanism | Cavitation + detergent chemistry | Solvent condensation/dissolution |
Blind holes, joints, complex parts | Excellent — cavitation reaches everywhere | Good where vapor reaches; line-of-sight less critical |
Particulate (chips, swarf) | Excellent — particles lifted and filtered out | Moderate — needs ultrasonic sump in the machine |
Chemistry handling | Water-based; wastewater treatment | Solvent containment, recovery, emissions control |
Throughput | Batch tanks to conveyor lines, scales widely | Compact machines; batch baskets |
Water-sensitive parts | Needs drying discipline | No water contact — an advantage |
Footprint & peripherals | Tanks, filtration, DI rinse, dryer | Sealed machine with solvent recovery |
Choosing for Your Parts
- Complex geometry, chips and water-tolerant materials → ultrasonic. Machined aluminum and steel, pre-plating cleaning, hydraulic components, moulds — the industrial default, and the route we build lines around: see ultrasonic cleaning machines.
- Water-sensitive assemblies, oils only, compact footprint → vapor degreasing earns its place; electronics and precision parts with trapped moisture concerns are its classic cases.
- Mixed reality → many plants run both: vapor degreasing for water-sensitive sub-assemblies, ultrasonic lines for everything else. Sequence matters: degrease first, then aqueous precision clean.
Field Workflow: Decide in Six Questions
- ☐ Is the soil oil-only, or oil + particles + paste?
- ☐ Does the part trap or fear water?
- ☐ Geometry: blind holes, joints, stacked surfaces?
- ☐ Material: solvents or detergents — any compatibility limits?
- ☐ Throughput: baskets per shift, and does it grow?
- ☐ Utilities: water treatment capacity vs solvent containment and recovery?
Standards and Evidence Boundary
- ASTM A380 — cleaning, descaling and passivation of stainless parts; ultrasonic cleaning is one of the recognized methods within such procedures.
- Chemistry supplier datasheets — detergent concentration, temperature and dwell windows (aqueous), or solvent system specifications (vapor), define the process.
Evidence boundary: this article compares the two routes at industry-general level. Cleaning validation for a specific part comes from a soil test and the chemistry supplier's datasheet — not from this page; no solvent or detergent brands are recommended.
FAQ
Is vapor degreasing being phased out?
Modern machines run sealed solvent systems with recovery and emission controls; whether a solvent route fits a site depends on local environmental rules and the chemistry chosen. Both routes remain in industrial use.
Can ultrasonic cleaning damage precision parts?
Only with wrong parameters — aggressive low-frequency cavitation on soft metals, over-long dwell. With matched frequency, chemistry and time, it is the standard for precision cleaning.
Which is faster per basket?
Cycle times overlap in practice; ultrasonic cycles run minutes and scale with soil, vapor cycles depend on condensation rate and part mass. Throughput planning needs the part, not a rule of thumb.
What does an ultrasonic line need besides the tank?
Filtration and oil removal, heated DI rinses, a dryer, and loading logic — the machine is one element of the flow.
Related Reading
- Pillar guide: How Does an Ultrasonic Cleaner Work? — the cavitation physics in depth.
- Water side: Distilled vs Deionized Water for Ultrasonic Cleaners — what goes in the tank and the rinse.
- Next step: browse ultrasonic cleaning machines to size the line.
Diagnostic CTA: What to Send Us — and What You Get Back
Send three inputs through our RFQ form:
- Your dirtiest parts — soil, material, geometry
- Throughput and cleanliness requirement
- Site utilities and constraints
ES-PRO returns: a cleaning route recommendation (including the honest answer when vapor degreasing fits better), a line configuration, a quotation, and an explicit list of open questions — we state what is missing rather than assuming it.
References & Authorities
- ASTM A380 — Standard practice for cleaning, descaling and passivation of stainless steel parts, systems and equipment — ASTM International.
- Chemistry supplier datasheets — detergent and solvent system specifications, concentrations and operating windows (issued by the chemistry supplier).
- Industry associations — e.g., NASF (National Association for Surface Finishing, US) and IMF (Institute of Materials Finishing, UK) publish supplementary guidance and training for the surface-finishing industry.
- Standards are cited for identification; always use the current edition from the issuing body. Process parameters are governed by the datasheets for the specific chemistry.


