Applications
Plating for Medical Devices: Materials, Cleanliness & Equipment
Medical device plating demands validated cleanliness and documented control. See coating choices for instruments, cleaning steps and equipment that supports validation.
Medical device plating is less about shine than documented cleanliness: validated cleaning, controlled deposits and traceable process records. About a 6-minute read.
Written by Nick Wong · Engineering reviewed by Li Wang · Published 4 October 2026 · Updated 4 October 2026
For medical manufacturers, surface finishing is a regulated process step, not a cosmetic one. Surgical instruments, trays and device components need finishes that survive repeated sterilization and cleaning chemistries, and the line that produces them has to prove — with records, not impressions — that every load was cleaned, plated or passivated to spec. That combination of chemistry control and documentation is what separates a medical-grade finishing line from a general industrial one.
What Medical Manufacturers Plate — and Why
Start with an accuracy point that saves confusion: implantable devices are usually not electroplated at all. Implants are typically made from titanium or cobalt-chrome and receive surface treatments (passivation, anodizing, coatings) rather than metallic electroplate. The plating demand in medical sits elsewhere:
- Surgical instruments — scissors, forceps, retractors — mostly stainless steel. The critical "finish" is often passivation (a chemical treatment that removes free iron and strengthens the natural chromium-oxide layer) rather than a deposited coating. Some instrument families receive electroless nickel or decorative/functional plating on non-cutting components.
- Instrument trays, handles and hardware — stainless or plated components that must survive thousands of autoclave and washer-disinfector cycles.
- Electrosurgical and powered device components — plated contacts, tips and connectors where gold or silver provides stable conductivity.
- Equipment and fixture hardware around the device itself, where corrosion resistance is the requirement.
The common thread: the finish has to perform after repeated reprocessing, and its absence — pitting, free iron, residue — is a rejection, not an aesthetic issue.
Cleanliness Is the Spec
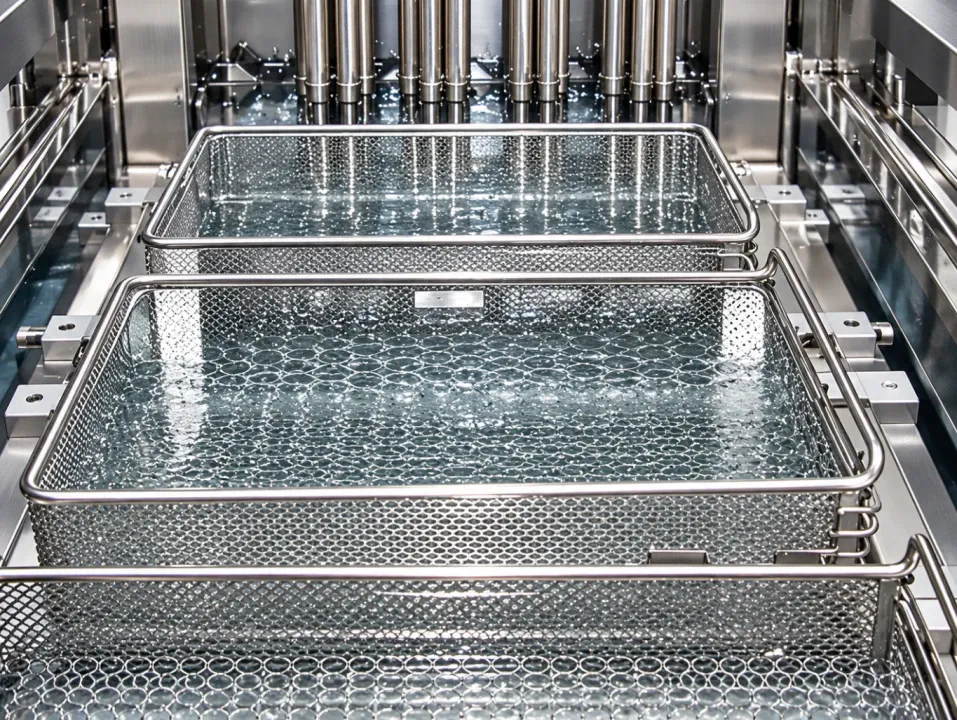
In general industry, cleaning is a pre-treatment step. In medical, cleaning is frequently the specification: a validated cleaning process with defined parameters is part of the product's regulatory file. Ultrasonic cleaning is the workhorse here, because cavitation reaches threads, box joints and serrations that spray and manual methods cannot — the same physics that drives how ultrasonic cleaning works, applied to instruments after use.
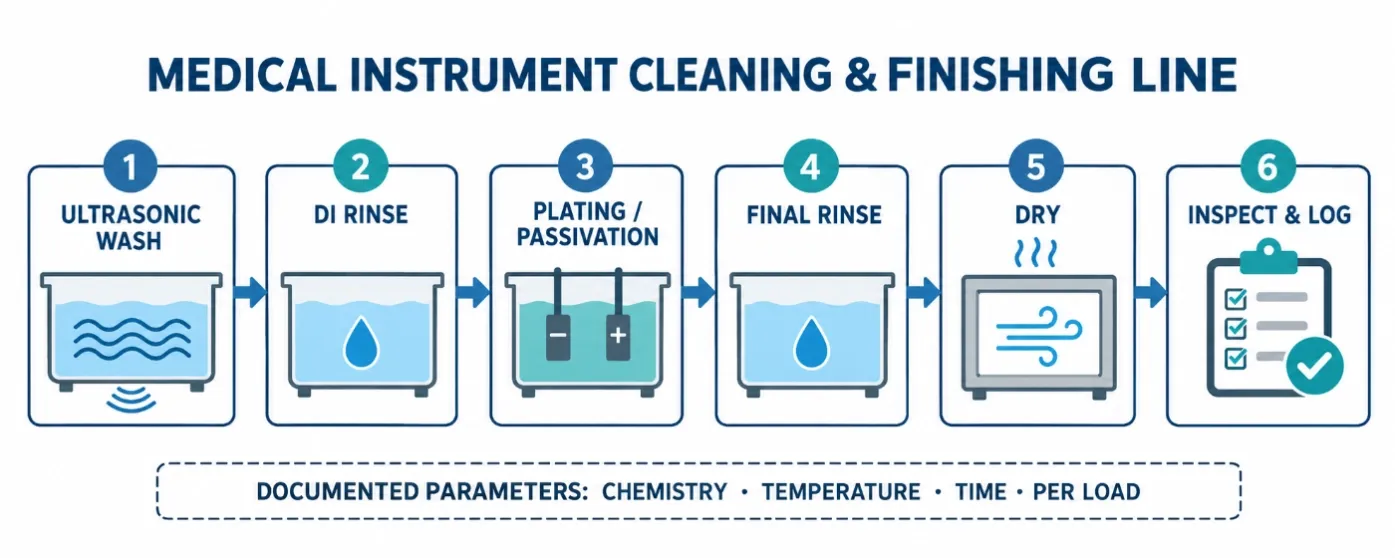
A medical-grade wash and rinse sequence is built to be repeatable and provable:
- Ultrasonic wash in a detergent matched to the soil (bioburden, polishing compounds, machining oils), at a documented concentration and temperature.
- Multi-stage DI rinsing — the last water touching the instrument should be the purest, so nothing dries onto the surface. On-site RO / DI water systems supply this continuously.
- Drying and inspection under controlled conditions, with the load identified and the cycle parameters logged.
Materials and Finishes: Reference Table
Component | Typical finish | Why | Watch-outs |
|---|---|---|---|
Stainless instruments | Passivation (citric or nitric) | Removes free iron; restores corrosion resistance after machining | Passivation ≠ plating: no thickness to hide bad surfaces |
Instrument trays / hardware | Electroless nickel | Uniform deposit on complex shapes; autoclave-cycle corrosion resistance | Phosphorus grade and bath windows come from the datasheet |
Electrosurgical contacts / connectors | Gold or silver plating | Stable low contact resistance over repeated cycles | Thickness and adhesion per the customer's component spec |
Device housings / fixtures | Nickel or tin plating | Corrosion protection, solderability where needed | Substrate preparation decides adhesion |
Implants | Usually surface-treated, not plated | Titanium/coCr biology | Do not quote plating where the industry doesn't use it |
Field Workflow: Building a Line That Can Be Validated
A validation-ready finishing line is designed backwards from the records a quality team will need. One reusable planning rule: every process parameter that appears in the product file must be set, held and logged by the line — not by an operator's memory.
Walk any proposed line against this checklist:
- ☐ Wash concentration and temperature controlled and logged per cycle
- ☐ Rinse water resistivity monitored on the final stage
- ☐ Bath chemistry (concentration, pH, temperature) dosed to datasheet windows and recorded
- ☐ Load identification (basket/rack ID) travels with the parts through the sequence
- ☐ Cycle time and tank sequence run by program, not by stopwatch
- ☐ Records exportable per load for the quality file
Standards and Evidence Boundary
References commonly cited around medical device finishing (always the current edition):
- ASTM A967 — chemical passivation of stainless steel parts; the standard anchor when an instrument spec says "passivated".
- ASTM F86 — surface preparation and marking of metallic surgical implants; the reference practice for implant surface condition.
- ISO 13485 — the medical-device quality-management framework; validation and documentation expectations flow from it. (Cited as industry context — not a claim of certification.)
Evidence boundary: this article states industry-general facts about finishing and cleaning for medical devices. Acceptance criteria, validation protocols and coating specs come from your regulatory file, customer drawings and the chemistry supplier's datasheets — not from this page, and no certification status is stated or implied here.
FAQ
Can you electroplate implants?
As a rule, no — implants are titanium or cobalt-chrome and receive surface treatments rather than metallic electroplate. Plating in medical is concentrated on instruments, trays, contacts and device components. Any implant-adjacent work follows the implant manufacturer's surface specification.
Why is ultrasonic cleaning preferred for instruments?
Cavitation reaches the geometries that defeat sprays and manual scrubbing — box joints, serrations, threads and cannulations — at a controlled, repeatable parameter set. That repeatability is what a validation file needs.
What does "validated" cleaning actually mean?
It means the cleaning process is proven to work and documented so it can be repeated: defined chemistry, concentration, temperature, time and rinse quality, with records showing each production cycle ran inside those limits.
Passivation or plating — which does my part need?
They solve different problems. Passivation cleans up stainless at a chemical level and adds no thickness; plating deposits a new metal layer for corrosion, conductivity or wear. The part's function and the customer spec decide — and many instrument lines need both, in the right order.
Related Reading
- Pillar guide: How Does an Ultrasonic Cleaner Work? — the cavitation physics behind validated instrument cleaning.
- Adjacent decision: What Is Electroplating? — the process fundamentals behind the deposits in the table above.
- Next step: browse industrial ultrasonic cleaning machines and plating lines.
Diagnostic CTA: What to Send Us — and What You Get Back
If you are specifying finishing or cleaning equipment for a medical product line, send three inputs through our RFQ form:
- The components and substrate — instruments, trays, contacts — and their finish targets
- The regulatory context: what records and parameters your quality file requires
- Throughput — baskets or racks per shift, and sterilization/reprocessing cycles the finish must survive
ES-PRO returns: a line configuration covering wash, rinse, plating/passivation and drying stages, a proposal for the documentation points (logging, resistivity monitoring, load traceability), a quotation, and an explicit list of open questions — we state what is missing rather than assuming it.
References & Authorities
- ASTM A967 — Standard specification for chemical passivation treatments for stainless steel parts — ASTM International.
- ASTM F86 — Standard practice for surface preparation and marking of metallic surgical implants — ASTM International.
- ISO 13485 — Medical devices — Quality management systems — Requirements for regulatory purposes — International Organization for Standardization (ISO).
- Chemistry supplier datasheets — detergent and bath concentrations, temperature windows and dwell times for the specific chemistry are defined by the chemistry supplier.
- Industry associations — e.g., NASF (National Association for Surface Finishing, US) and IMF (Institute of Materials Finishing, UK) publish supplementary guidance and training for the surface-finishing industry.
- Standards are cited for identification; always use the current edition from the issuing body. Process parameters are governed by the datasheets for the specific chemistry.