
Plating Process
Pickling Descaling Steel Pretreatment Equipment
Pickling and descaling are the first steps in any steel plating line — they remove the oxide scale, rust and mill surface that would otherwise prevent adhesion. A poorly specified pickling line causes
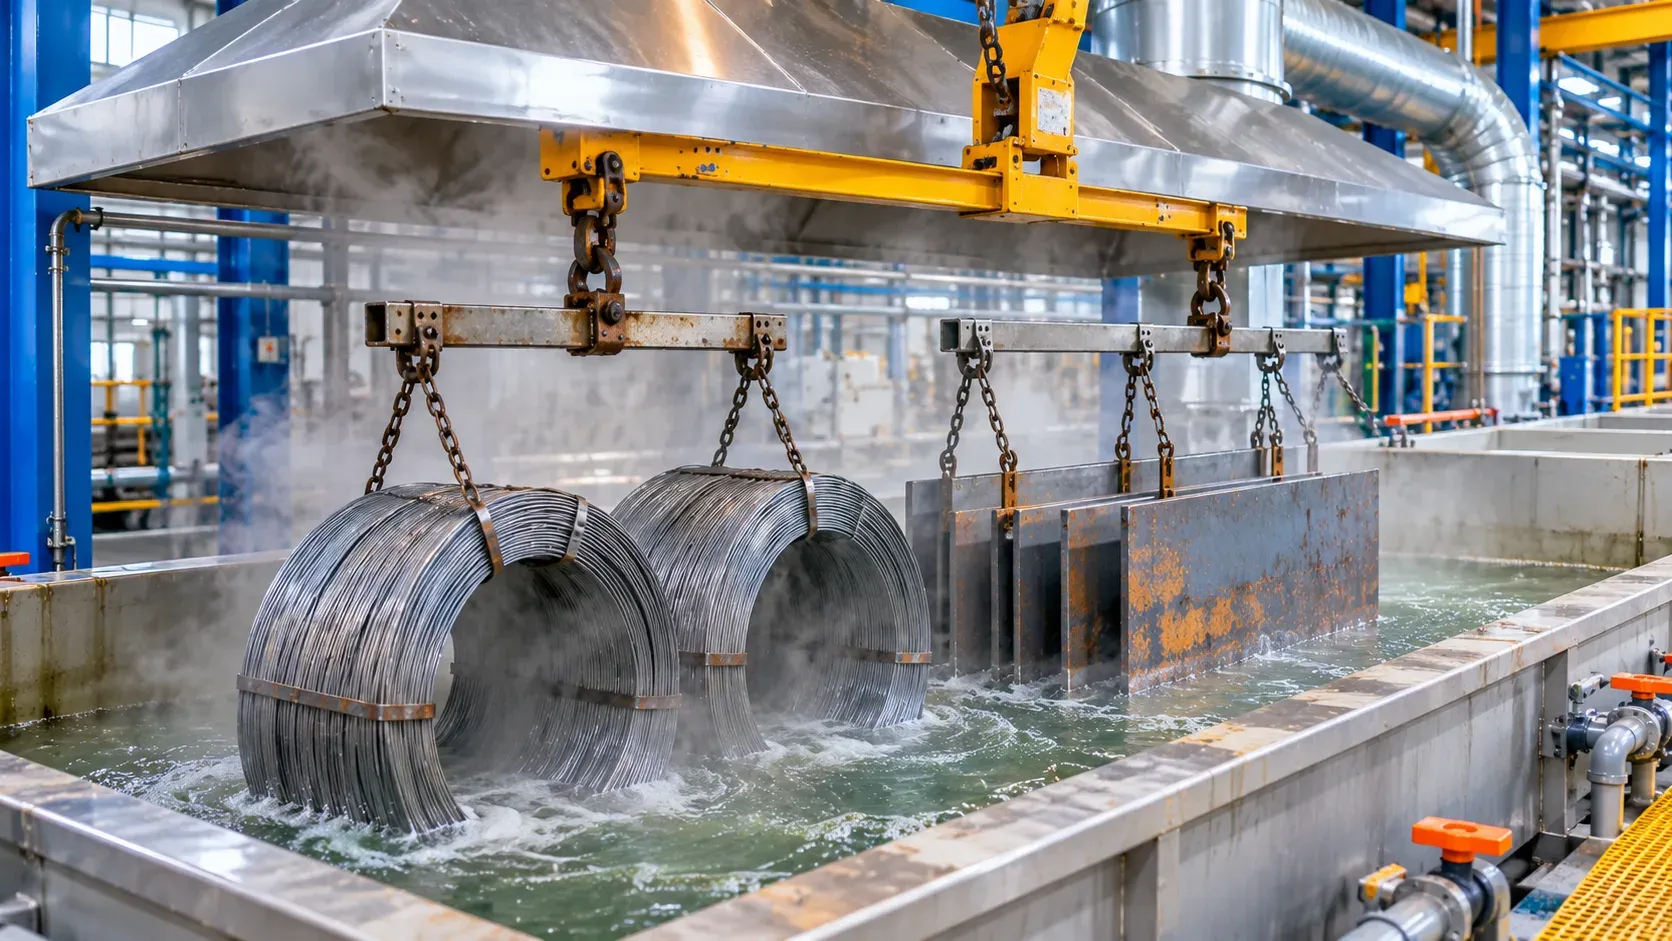
Pickling and descaling are the first steps in any steel plating line — they remove the oxide scale, rust and mill surface that would otherwise prevent adhesion. A poorly specified pickling line causes more downstream quality problems than any other stage, because residual oxide is invisible after plating but shows up as adhesion failure. This guide covers the equipment scope for a steel pre-treatment pickling stage.
Technical planning document — confirm acid concentrations and temperatures with your chemistry supplier.
What pickling removes and why it matters
Steel arrives at the plating line with one or more surface contaminants: mill scale (iron oxide layers from hot rolling), rust from storage, heat-treat scale, welding scale or machining oils. Pickling uses an acid bath — typically hydrochloric or sulfuric — to dissolve these oxides chemically. If any oxide remains after pickling, the electroplated coating deposits on oxide instead of on clean steel, and the adhesion test will find it.
Pickling acid selection
Acid | Concentration | Temperature | Best for | Considerations |
|---|---|---|---|---|
Hydrochloric (HCl) | 10–20% | Room temperature to 40°C | Most common — fast scale removal | Fumes require extraction; short bath life; low cost |
Sulfuric (H₂SO₄) | 10–25% | 60–80°C | Heavy scale; hot-rolled steel | Higher temperature needed; longer bath life |
Phosphoric | 15–25% | Room to 60°C | Light rust; leaves a phosphate layer that aids plating | Slower; more expensive; less fume |
Hydrochloric acid at room temperature is the most common choice for plating-line pickling. Sulfuric at elevated temperature is used for heavy mill scale. Phosphoric is used where a phosphate conversion layer is wanted before plating.
Equipment scope
Item | What to specify |
|---|---|
Pickling tank | PP, PVC or fibreglass; sized for the largest part plus fixture; heated if using sulfuric |
Fume extraction | Lateral exhaust or covered tank — HCl fumes are aggressive and corrosive to the building |
Acid scrubber | Packed-bed or mesh mist eliminator for the extraction stream |
Inhibitor dosing | Pickling inhibitor prevents acid attack on clean steel while oxide dissolves — dosing system required |
Agitation | Solution movement or part movement to clear acid from recesses and refresh the boundary layer |
Rinse | Counterflow rinse after pickling — acid carry-over contaminates the next stage |
Neutralisation | Mild alkaline dip or rinse to neutralize acid before the next stage |
Effluent | Acid rinse water with dissolved iron — treatment before discharge |
Bath monitoring | Acid concentration and iron content titration or instrumented monitoring |
For the rinse design that limits acid carry-over, see the rinse conductivity guide. For the effluent treatment of acid rinse water, see the wastewater treatment brief.
Inhibitors: why they matter
Pickling acid attacks both the oxide scale and the clean steel underneath it. Once the oxide is dissolved, the acid starts eating the base metal, generating hydrogen and roughening the surface. Pickling inhibitors are organic additives that adsorb onto the clean steel surface and slow acid attack there, while still allowing the oxide to dissolve. The right inhibitor reduces metal loss, hydrogen embrittlement risk and surface roughening.
Specify inhibitor dosing as part of the equipment scope — an automated dosing pump with a calibration check is more reliable than manual addition.
Common failure modes
- Over-pickling. Parts left in acid too long become rough and pitted, and absorb hydrogen. A timer on the hoist or a visual check protocol prevents this.
- Under-pickling. Oxide left in recesses causes adhesion failure downstream. Agitation and adequate acid concentration prevent this.
- Acid carry-over. Acid dragged into the next tank changes its chemistry. Counterflow rinsing and a drain timer on the hoist prevent this.
- Exhaust system corrosion. HCl fumes attack the extraction ductwork — PP or fibreglass ducting, not steel.
Key takeaways
- Pickling removes oxide that would cause adhesion failure — it is the foundation of the pre-treatment sequence.
- HCl at room temperature is the common choice; sulfuric at temperature for heavy scale.
- Pickling inhibitors reduce metal loss, hydrogen absorption and surface roughening.
- Fume extraction in PP or fibreglass is mandatory for HCl — steel ducts will corrode.
- Counterflow rinsing after pickling prevents acid carry-over that contaminates downstream stages.
Your next five steps
- Characterise the scale and rust on your incoming steel — thickness and type.
- Select the acid chemistry based on scale type, production volume and budget.
- Specify inhibitor dosing, agitation and fume extraction as part of the tank scope.
- Design the rinse stage to prevent acid carry-over into the electrocleaner.
- Set a bath monitoring routine for acid concentration and dissolved iron.
FAQ
Can we pickle without inhibitors?
Technically yes, but the clean steel will be attacked after the oxide dissolves. Inhibitors reduce metal loss, hydrogen absorption and surface roughening — especially important for high-strength steels and precision parts.
How long does a pickling bath last?
HCl baths are exhausted when the acid concentration drops below the effective range and the dissolved iron content rises. Titration tells you when to dump and recharge. Bath life depends on production volume and drag-out rate.
Why is HCl fume extraction so aggressive on ductwork?
HCl fumes form hydrochloric acid condensation that attacks most metals. PP or fibreglass ducting is the standard material — steel ducts will corrode through within months.
Image note: AI-generated editorial photography illustrates equipment or workpiece contexts; it is not an ES-PRO installation, customer reference or evidence of coating performance.


