Plating Lines & Equipment
Decorative Nickel Chrome Plating System
The nickel-chrome decorative plating system has been the standard for automotive trim, bathroom fittings, appliances and furniture hardware for over 90 years. The system is a multi-layer stack — coppe
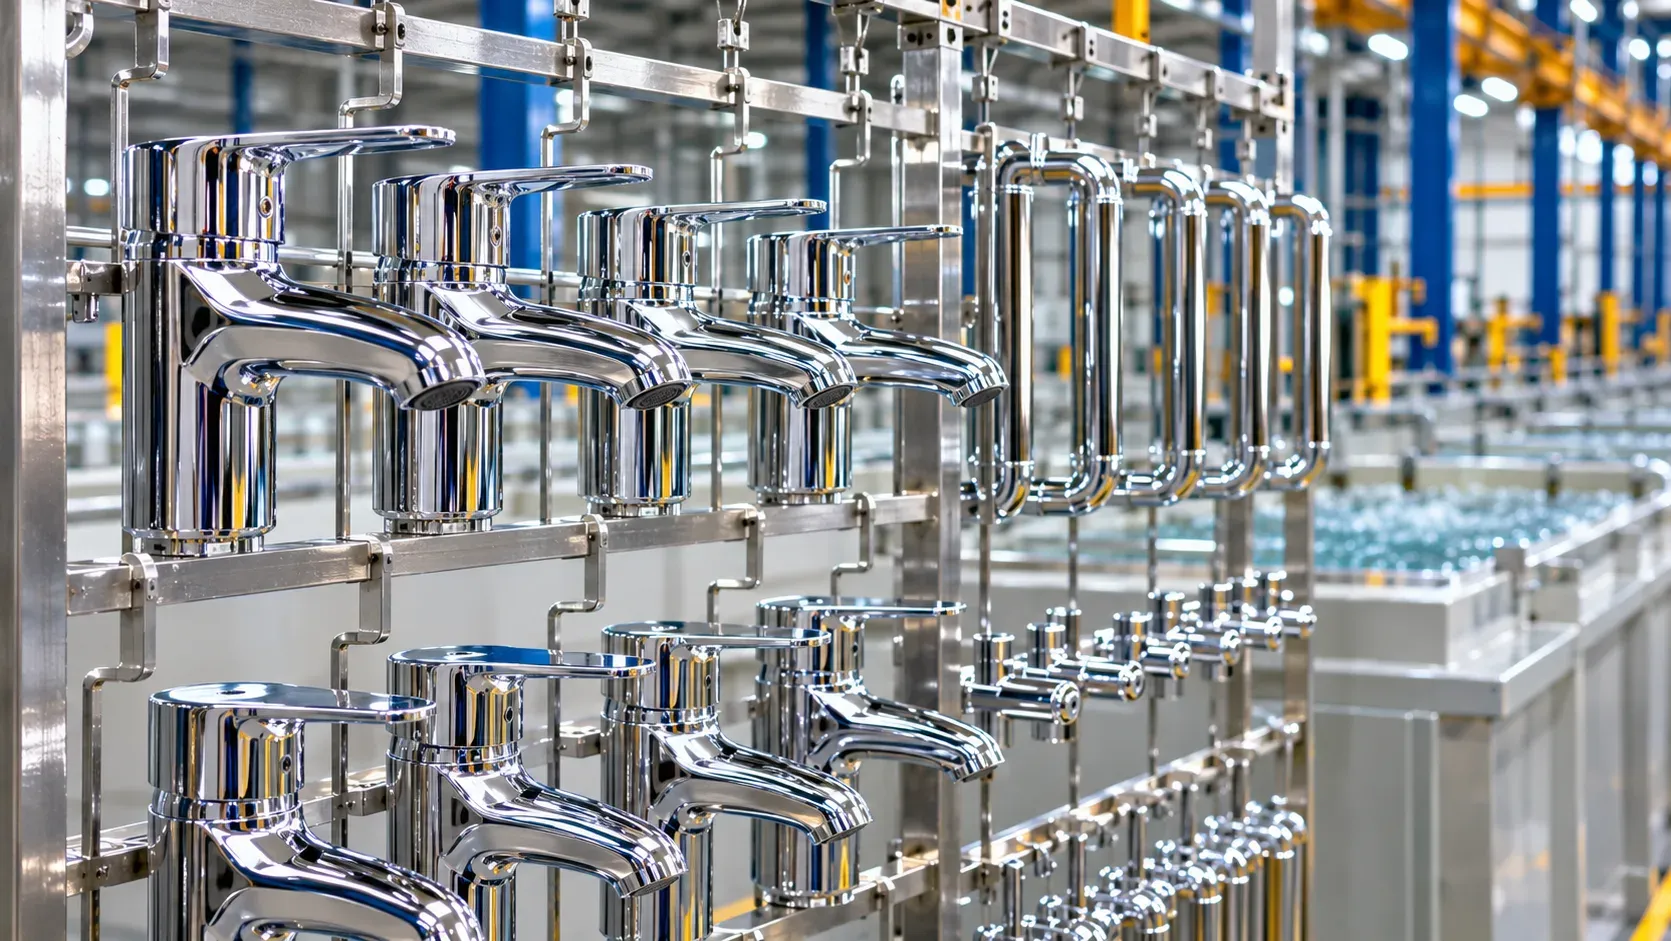
The nickel-chrome decorative plating system has been the standard for automotive trim, bathroom fittings, appliances and furniture hardware for over 90 years. The system is a multi-layer stack — copper, semi-bright nickel, bright nickel, micro-porous chrome — where each layer serves a specific corrosion protection or appearance function. This guide covers the system architecture, the equipment scope per layer, and the specification points that separate a quality installation from a short-lived one.
Technical planning document — confirm layer thicknesses and chemistry parameters with your chemistry supplier.
The multi-layer stack
Layer | Thickness | Function | Chemistry |
|---|---|---|---|
Copper strike | 1–3 µm | Adhesion layer on steel or zinc; levels the substrate | Cyanide copper or acid copper |
Copper build (optional) | 5–20 µm | Levels surface roughness; improves corrosion resistance | Acid copper sulfate with brighteners |
Semi-bright nickel | 10–20 µm | Primary corrosion barrier — sulfur-free, columnar structure | Watts nickel without sulfur-containing brighteners |
Bright nickel | 5–10 µm | Provides brightness; electrochemically active layer | Watts nickel with sulfur-containing brighteners |
Micro-porous chrome | 0.25–0.5 µm | Top layer — micro-porous structure disperses corrosion cells | Trivalent or hexavalent chrome with special plating technique |
The corrosion protection comes from the interaction between the semi-bright and bright nickel layers: the bright nickel corrodes preferentially, protecting the semi-bright layer and the substrate. This "sacrificial" mechanism is the reason the multi-layer system outperforms a single nickel layer of the same total thickness.
Equipment scope per layer
Tank | Chemistry | Temperature | Rectifier | Special equipment |
|---|---|---|---|---|
Copper strike | Cyanide copper | 40–50°C | Low current density | Cyanide destruct in effluent treatment |
Acid copper | Copper sulfate + brighteners | Room–30°C | Medium current density | Anode bags, filtration, bath analysis |
Semi-bright nickel | Watts nickel (no sulfur brightener) | 55–60°C | Standard | Separate tank from bright nickel — no cross-contamination |
Bright nickel | Watts nickel + brighteners | 55–60°C | Standard | Brightener dosing system, Hull cell for bath control |
Chrome | Trivalent or hexavalent | 45–55°C | High current density | Micro-porous nickel pre-layer for micro-porous chrome |
The tank materials guide covers the material selection for each chemistry; the rectifier load guide covers the power supply sizing.
The specification points that separate quality from shortcuts
- Semi-bright nickel must be sulfur-free. If sulfur-containing brighteners leak into the semi-bright bath, the sacrificial mechanism is destroyed. Separate tanks with dedicated filtration and no shared equipment.
- Layer thickness ratios matter. The semi-bright layer must be thicker than the bright nickel layer. A common specification is 2:1 or 3:1 (semi-bright:bright). Too thin a semi-bright layer defeats the corrosion protection.
- Micro-porous chrome extends life. The micro-porous chrome layer (created by plating chrome over a micro-porous nickel layer) disperses the corrosion current across thousands of micro-cells, preventing concentrated pitting.
- Copper build is optional but improves corrosion resistance. A copper layer between the strike and the nickel adds levelling and corrosion protection — particularly important on zinc die castings.
Key takeaways
- The corrosion protection is multi-layer chemistry, not just thickness — each layer has a defined role.
- Semi-bright nickel is the primary barrier and must be sulfur-free.
- Micro-porous chrome disperses corrosion current and is the modern decorative top layer.
- The equipment scope is a multi-tank line with separate nickel baths and specific chemistry controls.
- Layer thickness ratio (semi-bright:bright) is a specification point that inspectors and OEM auditors check.
Your next five steps
- Define the substrate (steel, zinc die casting, brass, aluminum) — it determines the strike chemistry.
- Specify the layer stack with thicknesses per your customer specification or industry standard.
- Size the tanks, rectifiers and filtration for each chemistry.
- Plan the effluent treatment for the mixed chemistry waste (cyanide, acid, nickel, chrome).
- Build a Hull cell testing routine for the bright nickel bath — brightener control is critical.
FAQ
Why can't we just use one thick nickel layer?
A single nickel layer of the same total thickness provides less corrosion protection than the dual-layer system. The electrochemical interaction between the sulfur-free and sulfur-containing layers creates a sacrificial mechanism that delays corrosion reaching the substrate.
What is the difference between semi-bright and bright nickel?
Semi-bright nickel is deposited without sulfur-containing brighteners, producing a columnar, low-sulfur structure that is more noble (corrosion resistant). Bright nickel uses sulfur-containing brighteners and has a different electrochemical potential — it corrodes preferentially, protecting the semi-bright layer.
Can we use trivalent chrome instead of hexavalent for the top layer?
Yes — trivalent chrome is now the industry default for new decorative lines. The color is slightly darker than hexavalent chrome, but the corrosion protection is equivalent for the thin decorative thickness range.
Image note: AI-generated editorial photography illustrates equipment or workpiece contexts; it is not an ES-PRO installation, customer reference or evidence of coating performance.