
Plating Process
Chrome Plating Defects: What to Record Before Changing Equipment
Record chrome plating defects with part identity, coating route, load location, timing and inspection evidence before changing equipment or process conditions.
@media (max-width:600px) { .espro-guide { font-size: 17px; } .espro-guide .comparison-scroll { overflow: visible; } .espro-guide table, .espro-guide tbody, .espro-guide tr, .espro-guide td { display: block; width: auto; } .espro-guide thead { display: none; } .espro-guide tr { border-bottom: 2px solid #d7e3f4; } .espro-guide td { padding: 12px 15px; } .espro-guide td:before { content: attr(data-label); display: block; color: #2454a6; font-size: 12px; font-weight: 700; margin-bottom: 5px; } .espro-guide .brief-flow { display: block; } .espro-guide .brief-flow span { display: block; margin-bottom: 10px; } }
Chrome plating defects should be investigated with a traceable record of the part, coating route, load position, operating history and inspection result. Record the defect before changing equipment or process conditions. A photograph helps describe appearance, but the location, timing and repeat pattern are needed to decide what evidence should be collected next.
Record the defectAssess the evidenceControlled trial
Original editorial enquiry framework. Conceptual inputs, not an engineered layout or measured result.
What should you record before changing a chrome plating process?
Identify the part, drawing revision, substrate and required coating system. State when the defect was found: after a coating stage, after rinsing, after subsequent finishing or during later service. Record the final condition in which it was inspected. These details help distinguish observations made at different points in the production route.
Preserve the relevant load identity and the available process records. Note what changed before the problem appeared, including parts, incoming condition, tooling, maintenance and operating sequence. Separate confirmed records from recollection. A change that coincides with a defect is useful evidence to investigate; coincidence alone does not establish the cause.
Why identify the chrome coating system before investigating defects?
Engineering chromium on a metal part and an appearance-led coating system need different specification discussions. Identify whether the chromium is part of a specified layer system and what lies beneath it. Include any prior coating or rework. An investigation based only on the word “chrome” can combine parts with different preparation and acceptance requirements.
The official ASTM B177/B177M engineering chromium guide and ASTM B456 decorative metal coating specification provide different requirement contexts. B456 excludes plastics in its public scope. For plastic parts, use the actual substrate-specific requirement and our plastic chrome-plating guide to frame the route.
How should chrome plating defect locations be mapped?
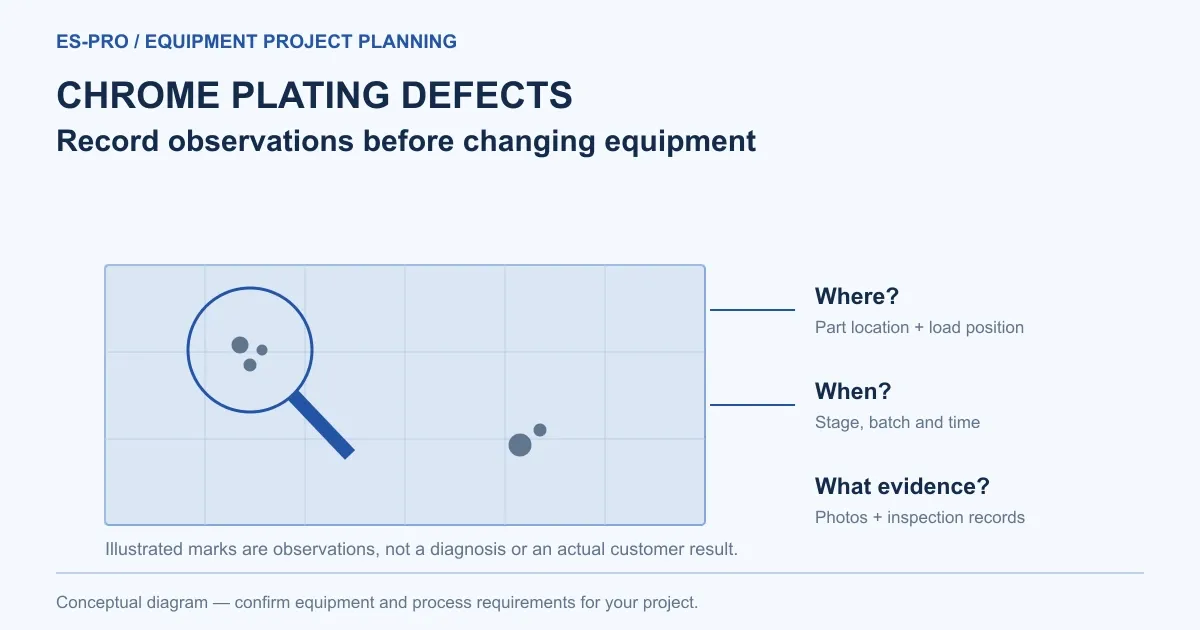
Mark the affected area on a drawing or annotated photograph. Include the contact location, orientation and position in the load where known. Record whether the condition appears on every part, one part family, one load position or an intermittent selection. Keep acceptable samples from the same production context available for comparison when the factory's procedures allow it.
Describe appearance using the inspector's agreed terminology. Avoid labelling a visible feature as a confirmed adhesion, thickness or contamination failure until the appropriate evidence supports that conclusion. Keep the observation and the proposed explanation in separate fields so an early assumption does not become the investigation's starting fact.
Record | What to capture | Decision it supports |
|---|---|---|
Part identity | Material, drawing and coating requirement | Select the relevant route and acceptance criteria |
Surface location | Marked defect and significant surfaces | Compare geometry and inspection positions |
Load context | Orientation, contacts and position | Check whether the pattern follows loading |
Timing | Stage at discovery and prior observations | Narrow the sequence requiring assessment |
Operating history | Available records and recent changes | Select evidence to examine before an alteration |
Inspection | Method, condition and result | Distinguish appearance from a demonstrated property |
This is an original investigation worksheet. It does not assign a chemical or equipment root cause from appearance alone.
What should be checked before changing chrome plating equipment?
Ask the process owner to review the approved route and the relevant production records. Identify which conditions are confirmed and which still need measurement. Check the actual load and tooling condition against the arrangement used in the proposal or previous accepted production. Record maintenance and interruption history where it may affect the assessment.
If equipment behaviour is questioned, state the observed behaviour and its timing. Ask what evidence would distinguish a control issue, a mechanical issue and a process change. Keep any proposed test within the factory's approved procedures. Avoid altering several unresolved variables together and then claiming that one hardware change corrected the coating problem.
How should tests be selected for chrome plating defects?
Use the part specification to choose the required test and specimen. Identify the inspection location and the condition before testing, including any later finishing operation. Record instrument and method information sufficient for the responsible inspector to assess the result. A photograph and a numerical measurement answer different questions and should remain linked to the same part identity.
The public ASTM B571-23 adhesion practice is relevant context for qualitative adhesion testing. It does not make one test suitable for every geometry or identify the cause of a failed result. Our thickness measurement guide provides related planning context for coating measurements.
What should a chrome plating corrective trial establish?
Write down the question the trial is intended to resolve. Identify the representative parts, approved operating conditions and inspection plan. Specify the proposed change and the records required before and afterwards. Agree who can approve the trial and who evaluates its outcome. Keep an unchanged comparison where the responsible process specialists judge it appropriate.
Record both the improvement observed and the limits of the conclusion. State which part family, load and conditions were assessed. If the defect is intermittent, agree what further evidence is needed before releasing a permanent modification. An acceptable sample supports the documented trial; it should not automatically become a guarantee for all subsequent production.
Questions You May Have:
Can a photograph establish why chrome is peeling?
It can document the visible condition and location. Root-cause assessment also needs the coating route, part history and appropriate inspection evidence; appearance alone is insufficient.
Should the first action be a new rectifier or agitation system?
Start with the recorded problem and the evidence needed to assess it. Request equipment assessment when the observed behaviour and investigation identify a relevant equipment question.
Are all chrome defect guides applicable to plastic parts?
No. Identify the substrate and complete layer system. Use the applicable specification and process-owner route rather than transferring a metal-part investigation unchanged.
What can I send when detailed process records are unavailable?
Provide the part, marked photographs, defect timing and known recent changes. Clearly identify missing records so the assessor can explain what information is needed next.
Get Proposal and Demo
Introduce your coating investigation with company, name, email and project country. Technical fields are optional. Share the marked defect location, part requirement and observed equipment behaviour when available. Ask which equipment assessment or controlled demonstration could address the specific question.
Send investigation documents by sales email, or chat on WhatsApp. Our equipment buyer's guide helps define the broader project boundary if a modification is subsequently justified.
Image note: AI-generated cover illustration; not an ES-PRO installation, customer project or test result.


