Applications
Automotive Plating: What OEM Approval Demands From a Line
Automotive plating lines are audited, not just bought. See what OEM approval expects — CQI-11 evidence, corrosion specs and the equipment that delivers both.
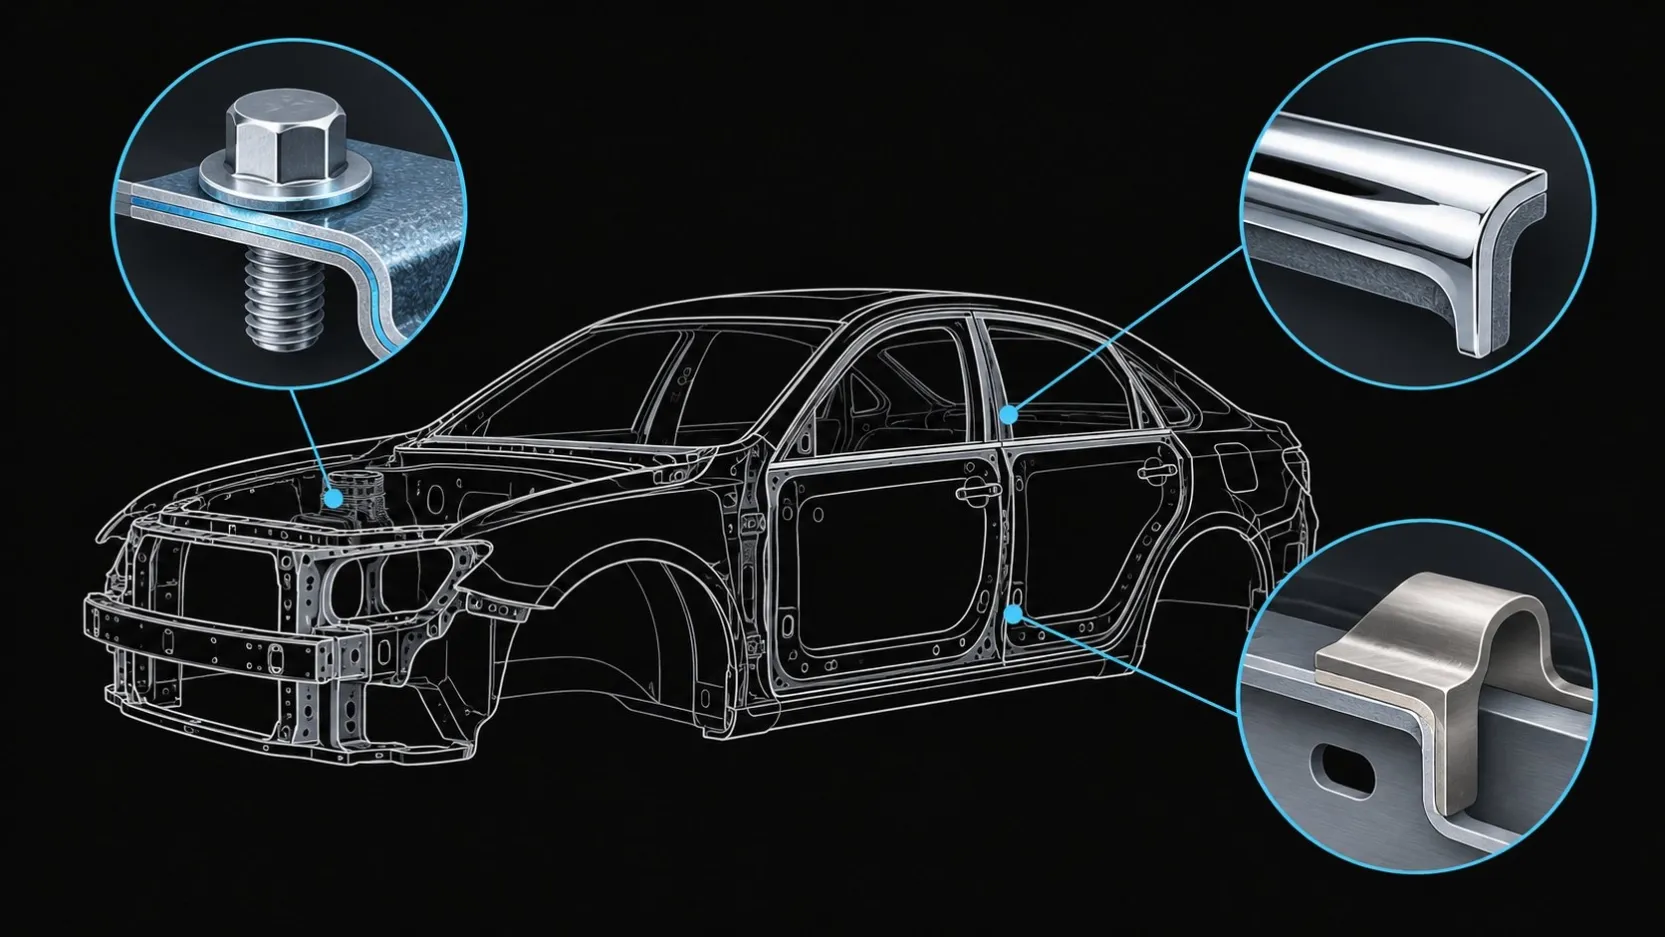
Automotive approval is earned by evidence, not equipment alone: a line that holds specs, logs every parameter and survives CQI-11-style audits. About a 6-minute read.
Written by Jason Han · Engineering reviewed by Eayon · Published 4 October 2026 · Updated 4 October 2026
Automotive customers do not approve a plating supplier the way they buy a machine. The approval attaches to the system: a line that holds its process parameters, produces the corrosion performance the drawing calls out, and can show records for every load it has run. That is why "automotive approved plating" is less a coating choice than an equipment-and-documentation requirement — and why the line design decisions matter as much as the chemistry.
What "Automotive Approved" Actually Means
Three frameworks sit behind the phrase:
- IATF 16949 — the automotive quality-management standard the customer's supply chain works under. It treats plating as a special process: one whose result cannot be fully verified by inspecting the part afterwards, so the process itself must be controlled and qualified.
- CQI-11 — the AIAG's Plating System Assessment, the self-assessment and audit framework automotive supply chains use specifically for electroplating. It walks through the plating system element by element: bath chemistry control, equipment maintenance, process monitoring, records.
- Customer-specific corrosion and coating specs — the drawing defines the coating system, thickness class and corrosion resistance the part must demonstrate.
None of these are certificates a line builder hands over. They define what the running line must be able to demonstrate, day after shift after shift — which is an equipment specification in disguise.
Corrosion Specs Drive the Line Design
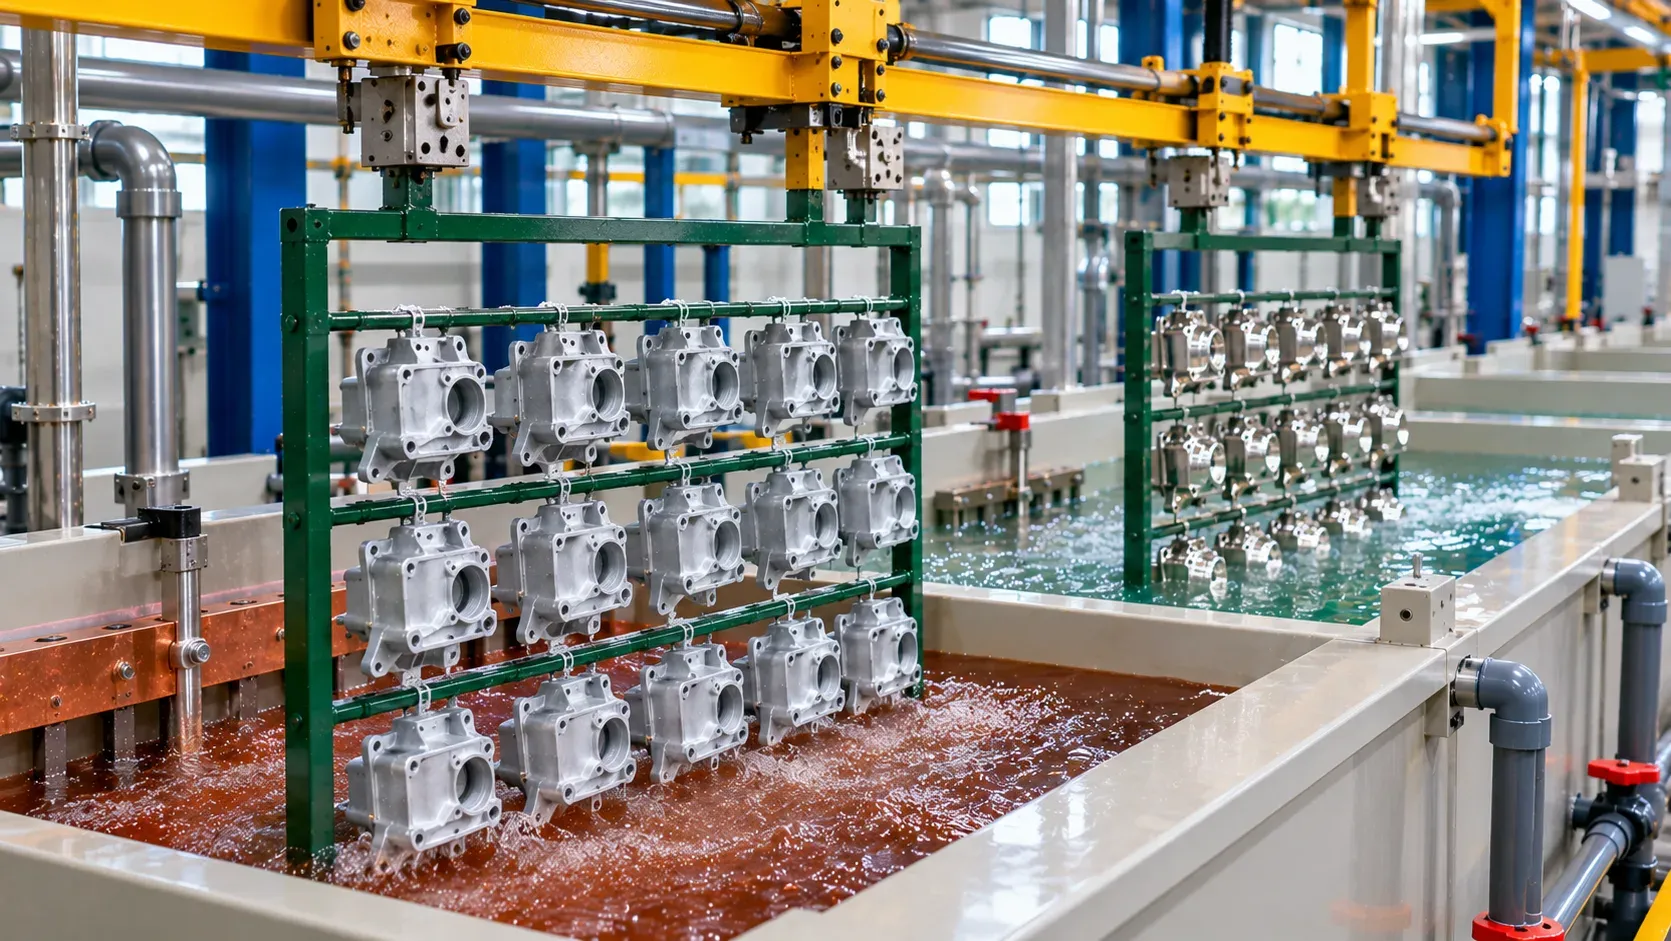
For chassis, fasteners and bracketry, the workhorse is zinc and zinc-alloy plating with a passivate, and the customer drawing decides the thickness class and corrosion resistance — zinc plating fundamentals covers the coating itself. What the drawing implies for the line:
- Thickness uniformity — the class must be met on the critical surfaces of every part, which pushes toward rack design, current-density control and shielding rather than "more amps".
- Passivate control — trivalent passivates are sensitive to concentration, temperature and contamination; the line has to dose and monitor them, not top them up by feel.
- Salt-spray performance — corrosion resistance is demonstrated by testing per ASTM B117 (the standard practice for operating a salt-spray apparatus); hours required come from the customer spec, and the line's consistency is what makes the demonstration repeatable.
- Hydrogen-embrittlement management — high-strength steels need baking schedules the line must run and record.
Equipment That Produces Evidence
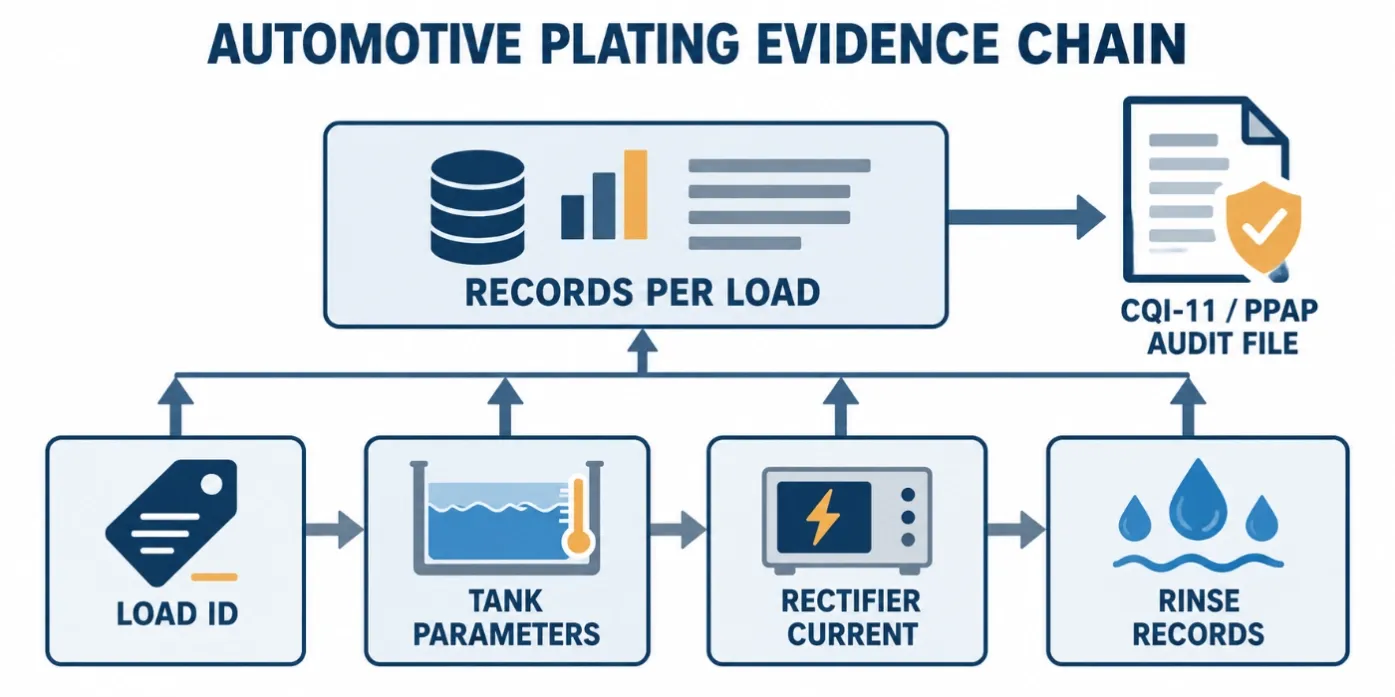
Every audit question ("show me this load's parameters") converts into an equipment feature:
Evidence the audit expects | What the line needs |
|---|---|
Bath chemistry inside datasheet windows | Dosing systems, concentration/pH/temperature monitoring with alarms, logged per cycle |
Correct current delivered per load | |
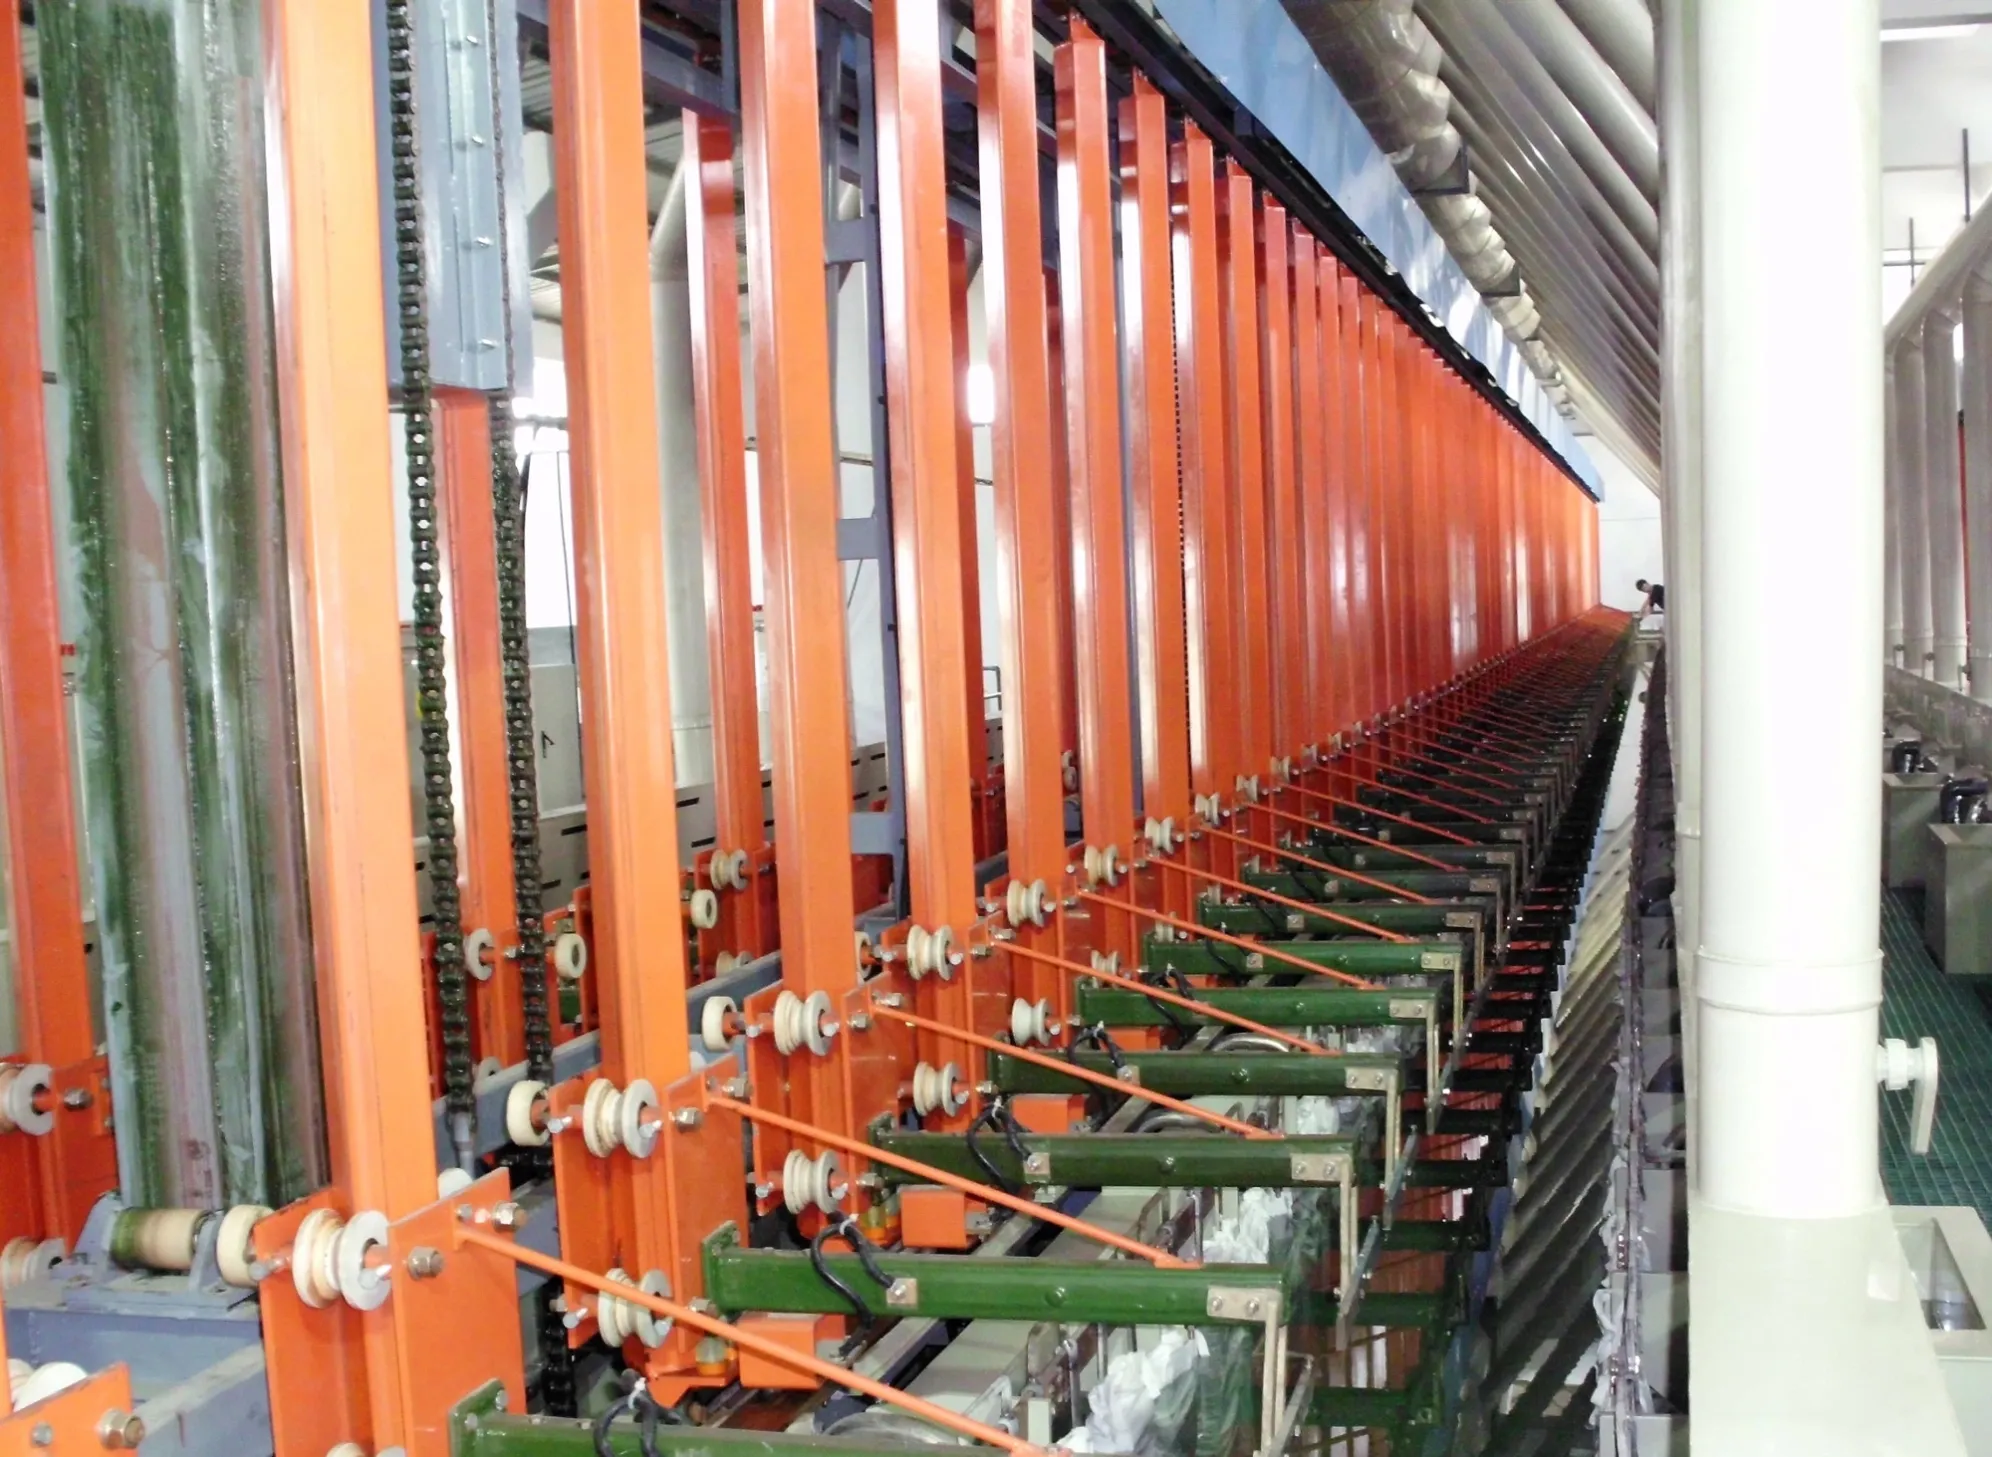
Identical sequence for every load | Programmable hoists and recipe control — not operator memory |
Rinse quality | Multi-stage counterflow rinses with final-stage resistivity monitoring |
Contamination control | Continuous filtration, oil removal, defined bath-analysis cadence |
Traceability | Load/rack ID carried through the sequence; records exportable per load |
Environmental compliance |
Field Workflow: Audit-Readiness Checklist
Before inviting an automotive audit onto a line, walk it against this list:
- ☐ Every parameter in the customer spec has a setpoint, an alarm and a log
- ☐ Bath analysis is scheduled by cadence, and results are filed per tank
- ☐ Rectifier output and cycle time are recorded per load, not per shift
- ☐ Passivate and rinse stages are monitored (concentration, temperature, resistivity)
- ☐ Maintenance on tanks, hoists and filters is scheduled and documented
- ☐ Rework and rejection paths are defined and recorded
- ☐ Wastewater and fume controls run inside permits, with monitoring records
Standards and Evidence Boundary
References commonly cited around automotive plating approval (always the current edition):
- CQI-11 — AIAG Special Process: Plating System Assessment; the audit framework automotive supply chains apply to electroplating.
- IATF 16949 — the automotive quality-management standard under which plating is treated as a special process.
- ASTM B633 / ISO 19598 — electrodeposited zinc coatings with thickness classes by service condition; the model for drawing-level coating specs.
- ASTM B117 — standard practice for operating salt-spray (fog) apparatus; the test method behind corrosion-resistance demonstrations.
Evidence boundary: this article describes what automotive approval frameworks expect of a plating line in general terms. Actual approval requirements, coating specs and corrosion hours come from your customer's drawings, the applicable standards and the audit framework your customer applies — not from this page. No certification status is stated or implied here on behalf of any party.
FAQ
We buy plated parts — does CQI-11 apply to us or to our plater?
The assessment applies to whoever runs the plating process. If plating is outsourced, the customer's flow-down typically reaches your plater — which is why buyer teams audit their suppliers' lines with CQI-11 as the reference.
Is a corrosion "hours of salt spray" figure the acceptance criterion?
The test method is general, the numbers are not: hours and pass-fail criteria come from the customer drawing and the coating spec it references. Design the line so the demonstration can be repeated on any production load.
Can a manual line pass an automotive approval?
Possibly, but the burden of proof shifts to records and operator discipline. Manual transport means the sequence repeatability and logging that audits expect must come from documentation rather than from recipe-controlled equipment — which is harder to sustain across shifts.
What records does a plating line produce per load?
At minimum: load ID, tank sequence and dwell times, bath temperatures and chemistry readings, rectifier current, rinse-stage status, and any deviations with disposition. The equipment's job is to generate these automatically.
Related Reading
- Adjacent decision: How to Set Up a Metal Plating Line — the equipment checklist this article's audit features come from.
- Coating fundamentals: Zinc Plating: Rust Protection, Process & Line Equipment — the workhorse automotive coating.
- Next step: browse plating lines to see automation levels and control options.
Diagnostic CTA: What to Send Us — and What You Get Back
If you are bringing a plating line toward automotive approval, send three inputs through our RFQ form:
- The coating systems and customer specs the line must satisfy (zinc/zinc-alloy classes, corrosion targets)
- Which approval framework your customer applies — and any audit findings you need to close
- Part mix, throughput and the records your quality system requires per load
ES-PRO returns: a line configuration with the control and logging points mapped to the audit expectations, an equipment list (rectification, dosing, filtration, rinsing, wastewater scope), a quotation, and an explicit list of open questions — we state what is missing rather than assuming it.
References & Authorities
- CQI-11 — Special Process: Plating System Assessment — Automotive Industry Action Group (AIAG).
- IATF 16949 — Quality management system requirements for automotive production organizations — International Automotive Task Force (IATF).
- ASTM B633 — Standard specification for electrodeposited coatings of zinc on iron and steel — ASTM International.
- ISO 19598 — Electroplated coatings of zinc and zinc alloys on iron or steel — International Organization for Standardization (ISO).
- ASTM B117 — Standard practice for operating salt spray (fog) apparatus — ASTM International.
- Chemistry supplier datasheets — bath systems, additive control and passivate windows for the specific chemistry are defined by the chemistry supplier.
- Industry associations — e.g., NASF (National Association for Surface Finishing, US) and IMF (Institute of Materials Finishing, UK) publish supplementary guidance and training for the surface-finishing industry.
- Standards are cited for identification; always use the current edition from the issuing body. Process parameters are governed by the datasheets for the specific chemistry.